Premium trophy programs often run into preventable disputes because buyer and factory teams use broad phrases such as no scratches, perfect finish, or luxury quality without defining what those terms mean in inspection practice. On a custom metal award, a mirror-plated front face, a recessed cast pattern, a painted insert, and a base underside cannot reasonably be judged by one vague rule. The practical solution is a shared appearance framework that defines trophy cosmetic defect standards by zone, finish, viewing distance, lighting, orientation, and approved references. As part of broader quality control, this alignment should happen before tooling approval, sample sign-off, and mass production, not after finished goods are on the table.
This guide is written for procurement managers, luxury-brand teams, executive-award buyers, and QA professionals who need a repeatable method for setting trophy cosmetic zones, award appearance inspection rules, trophy scratch defect limit expectations, and plating cosmetic acceptance criteria. The goal is not to claim one universal premium trophy quality standard. It is to help buyers and manufacturers jointly define project-specific acceptance criteria that fit the design intent, finish route, and real display conditions.
Why One Cosmetic Standard Cannot Fit Every Surface
A premium trophy is usually a mix of different geometries and finishing processes. Even when the end customer sees one elegant award, the manufacturer sees multiple appearance systems that behave differently in production and inspection.
- Polished metal faces reflect light strongly and make fine scratches, swirl marks, and plating waviness easier to see.
- Recessed cast details may naturally show more texture because draft angles, tool geometry, and access for polishing are limited.
- Plated edges can reveal sharp transitions, edge build-up, or tone variation differently from broad flat faces.
- Painted inserts are sensitive to color consistency, dust inclusions, edge coverage, and gloss mismatch.
- Engraved areas require separate checks for alignment, clarity, depth appearance, and burr-free presentation.
- Underside surfaces usually do not need the same visual standard as the front display face.
- Base-bottom contact areas need practical rules focused on function and handling rather than showroom presentation.
Process route matters just as much as geometry. Die casting may leave characteristics that require controlled removal or acceptance planning. Polishing can improve surface brilliance but may also introduce directional lines or edge softening if not matched to the design. Electroplating can change reflectivity, highlight substrate imperfections, and create sensitivity to handling marks, especially on electroplated trophies. Painting adds another appearance layer with its own acceptance criteria. Engraving and assembly introduce fit, registration, and cleanliness risks that do not belong in a simple scratch-only standard.
For that reason, a premium trophy quality standard should be surface-specific and process-aware. Buyers should not assume that a perfect product photo defines manufacturable appearance on every hidden edge and every angle. Instead, the development phase should identify which surfaces are critical, which process characteristics are unavoidable, and which visual outcomes must be confirmed by approved samples.
Map Hero, Secondary, Hidden, and Contact Zones
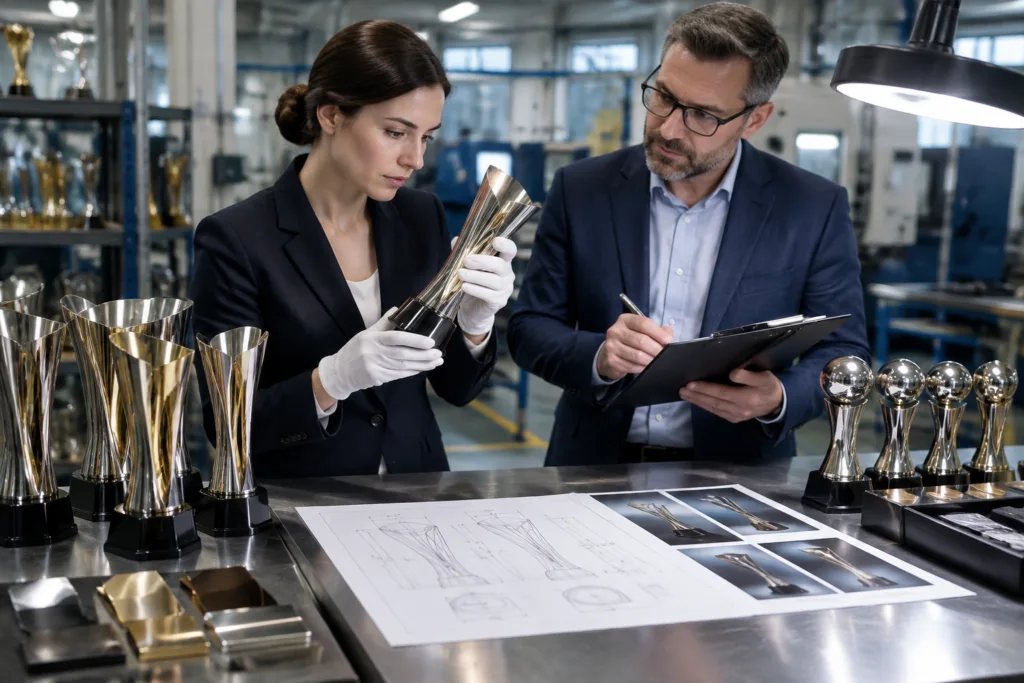
The most practical way to define trophy cosmetic zones is to classify every visible area of the award into inspection zones. A zone map turns subjective language into a shared decision tool.
Hero zones
Hero zones are the main brand-facing and camera-facing surfaces. These are typically the front display face, prominent logo panel, central sculpture face, and other surfaces most likely to attract immediate attention in unboxing, ceremony presentation, photography, and office display. Hero zones usually receive the strictest trophy cosmetic defect standards because defects here are most likely to affect perceived value.
Secondary zones
Secondary zones are visible in normal handling or side viewing, but they are not the primary focal point. Examples include sidewalls, rear shoulders, outer base sides, and non-primary decorative elements. These zones still matter for a premium feel, but their defect limits may be more practical than those for hero zones.
Hidden zones
Hidden zones are rarely seen in standard display orientation. These may include the underside of the award head, inner recesses, back-facing assembly interfaces, or shielded surfaces. Hidden does not mean uncontrolled; it means acceptance should match realistic use and access limitations.
Contact zones
Contact zones are areas likely to touch packaging, protective films, tables, gloves, or hands during production, packing, transport, and presentation. Base bottoms, felted contact faces, concealed support points, and handling edges often belong here. These surfaces need practical standards that consider friction, transport risk, and function.
For each SKU, buyers should request a cosmetic-zone drawing with front view, side view, top view, and close-up callouts for important features. If the trophy has mixed finishes, each finish should be marked by zone. If the trophy has removable parts or a presentation case, the orientation in the case should also be considered. In many programs, the strictest premium trophy quality standard applies to hero zones, but exact pass/fail requirements must be agreed per project and confirmed against actual samples.
Set Viewing Distance, Lighting, and Orientation
Many appearance disputes are not about the defect itself. They are about the conditions under which the defect was judged. A repeatable award appearance inspection standard therefore needs agreed inspection conditions before sample approval and bulk inspection begin.
- Viewing distance: Define the normal review distance for each zone and whether any close-range review is allowed for specific features.
- Observation time: Specify whether the inspector rotates the trophy briefly or studies each zone for an extended period.
- Orientation: Document the normal display angle, hand-held review angle, and any special camera-facing orientation.
- Lighting environment: State the type of light used for approval and final inspection, especially for reflective or dark finishes.
Different finishes react very differently under light. Mirror polishing and bright plating can amplify fine lines and dust. Brushed finishes may hide random marks but show directional inconsistency. Matte paint may reduce reflection but reveal particle contamination. Textured cast surfaces can mask small irregularities while emphasizing edge build-up. This is why good surface preparation planning must be paired with inspection-condition planning.
Buyers should decide whether acceptance is based on realistic use viewing or forensic close-range inspection. If a senior executive will see the award from desk distance under office lighting, that should be reflected in the acceptance framework. If the trophy will be used in close-up broadcast photography, hero zones may require more demanding evaluation. The important point is consistency. Borderline marks become costly arguments when no one agreed whether the product would be judged at normal display distance or under intense near-range scrutiny.
Classify Scratches, Pits, Dust, Color, and Assembly Gaps
Once zones and viewing conditions are defined, the next step is defect taxonomy. A good appearance standard does not say only no defects. It lists the defect types that matter and explains how they will be judged by zone and finish.
Surface-mark defects
- Linear scratches: Isolated straight or curved marks that interrupt reflectivity or paint continuity.
- Swirl marks: Fine circular or directional polishing traces, often more visible on gloss metal faces.
- Polishing waves: Uneven flatness or distortion caused by polishing or substrate irregularity.
For a mirror-plated front face, the trophy scratch defect limit may need to be much stricter than for a recessed texture. The same mark that is unacceptable in a hero zone may be acceptable in a hidden area under the agreed conditions.
Substrate and plating defects
- Casting pits: Small voids or surface disruptions visible after polishing or plating.
- Plating nodules: Raised points or irregular build-up that disturb reflectivity.
- Edge coverage issues: Thin appearance, tone inconsistency, or visible transition around edges and corners.
Plating cosmetic acceptance should therefore be linked to both substrate condition and final finish. A plated surface cannot hide every underlying imperfection, particularly on highly reflective faces.
Paint and color defects
- Dust in clear coat or paint: Visible trapped particles under the finish.
- Color variation: Perceived difference in hue, depth, or gloss between parts or batches.
- Coverage inconsistency: Thin edges, paint pooling, or uneven masking lines.
On projects using custom paint and color finishes, the inspection plan should identify which areas require exact visual matching and which can accept slight process variation, subject to project confirmation.
Decoration and assembly defects
- Engraving misalignment: Text or graphics positioned incorrectly relative to the approved artwork or datum.
- Logo placement deviation: Insert, badge, or print not centered or not level as expected.
- Adhesive visibility: Glue squeeze-out or residue visible at normal viewing angles.
- Assembly gaps: Visible separation at joints, especially on metal-to-base interfaces.
- Wobble: Instability when placed on a flat surface.
- Mixed-finish inconsistency: Poor visual harmony between polished, plated, painted, brushed, or textured areas.
Assembly joints often need their own fit-and-finish rules because they combine dimensional fit, cosmetic presentation, and functional stability. Exact numeric limits, sample counts, and rejection thresholds should not be assumed. They must be jointly defined and approved for each program.
| Defect type | Usually most sensitive in | Needs separate rule by finish? |
|---|---|---|
| Scratch or swirl | Hero mirror faces | Yes |
| Casting pit | Broad plated faces | Yes |
| Dust in paint | Solid color inserts | Yes |
| Engraving alignment | Nameplates and logos | Usually |
| Assembly gap | Metal-to-base joints | Yes |
| Wobble | Base contact surfaces | No, but zone-specific |
Use Limit Samples and Approved Masters
Words alone rarely settle borderline visual calls. A stronger method is to build an approval package that includes a golden sample, approved master, retain sample set, and limit samples showing acceptable and non-acceptable conditions.
- Golden sample: The main visual reference approved by the buyer for design intent and overall finish.
- Approved master: The production reference held for factory and inspector comparison.
- Retain samples: Reference units stored for future order comparison and dispute review.
- Limit samples: Borderline examples that show what is still acceptable and what must be rejected.
Limit samples are especially valuable for cosmetic calls such as fine scratch visibility, plating tone range, paint particle visibility, engraving appearance, and assembly alignment. They reduce subjective debate much better than generic wording because the buyer, factory, and third-party inspector can compare against the same physical benchmark.
A robust package should also document finish references for plating tone, polish level, paint color, engraved look, and part-to-part alignment. Ideally, these references are tied to revision control so every sample, pilot run, and reorder is judged against the current approved version. For custom trophy programs, Me Trophy can support sample production and appearance alignment during development, while exact workflow details, review checkpoints, and sample-handling responsibilities must be confirmed for the project.
Train Inspectors and Control Reorder Consistency
Even a well-written standard fails if inspectors do not apply it consistently. Appearance criteria should therefore be translated into training, station references, in-process checks, final inspection routines, and reorder controls.
At the production level, teams should confirm which defects are checked after casting, after polishing, after plating, after painting, after engraving, after assembly, and before packing. Catching a problem only at the end of line is expensive and less reliable than controlling appearance step by step.
- Inspector training: Use real approved samples and limit samples, not only verbal instructions.
- Photo standards: Mark zones and show examples of acceptable and unacceptable conditions.
- Station references: Place process-specific appearance references where work is performed.
- Change control: Record updates to mold, polishing method, plating source, paint system, adhesive method, and packaging configuration.
- Reorder review: Confirm whether the same approved sample and defect limits govern replenishment orders.
This is where appearance management connects back to the broader quality control pillar. A strong cosmetic standard is not only an end-of-line sorting tool. It is a process-control system. If tooling is modified, a plating chemistry source changes, or packaging contact points are redesigned, reorder consistency should be revalidated against the approved appearance standard.
Key Procurement Questions to Resolve Before PO Approval
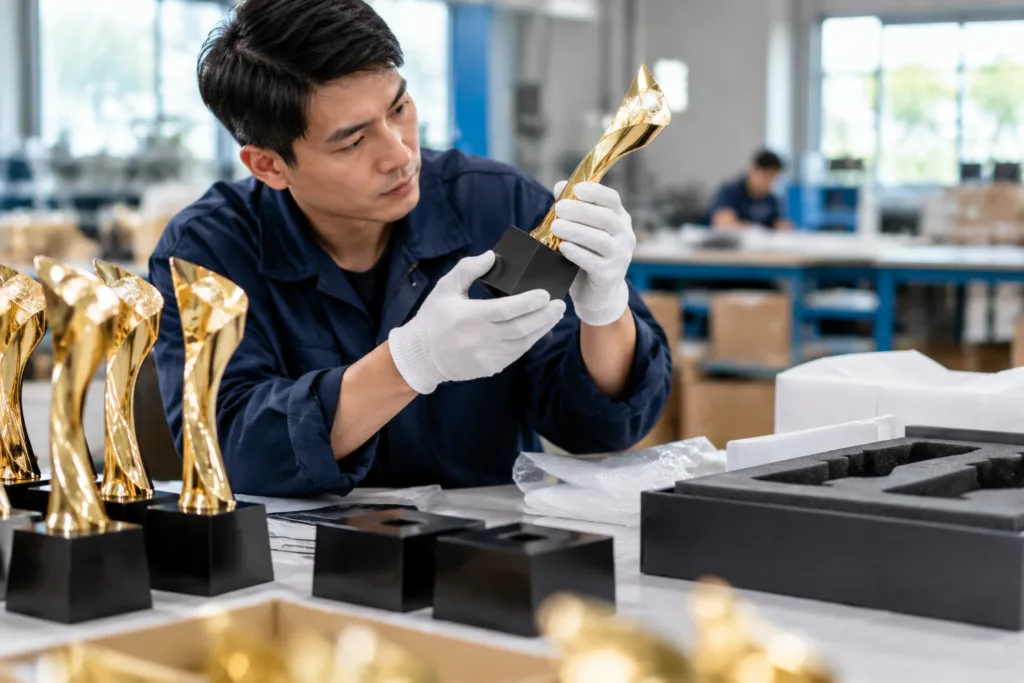
Before issuing a purchase order, buyers should make sure the specification package answers the commercial and technical questions that most often cause later disagreement.
- Which surfaces are hero zones, and which are secondary, hidden, or contact zones?
- Which finish is most defect-sensitive in this design: mirror polish, bright plating, brushed metal, matte paint, or mixed finish?
- What are the agreed viewing distance, lighting type, observation time, and trophy orientation?
- How will borderline defects be decided: by written rule, by approved master, or by limit sample comparison?
- Which sample governs reorders if multiple development samples exist?
- Who signs off if tooling, plating tone, paint batch, or assembly method changes?
- What packaging protections are required to preserve approved appearance during export delivery?
These questions are especially important for international OEM and ODM projects where design, sourcing, manufacturing, and approval may happen across different teams and countries. If your team needs to align appearance criteria before tooling and bulk production, it is better to resolve the specification logic early than to rely on post-production negotiation.
Recommended Asset and Documentation Package
For premium trophy projects, buyers should request or prepare a documentation set that can travel with the product through development, sampling, pilot production, mass production, and repeat orders.
Core documents
- Cosmetic-zone drawing: Front, side, top, and detail views with zone classification.
- Appearance specification sheet: Finish map, inspection conditions, defect categories, and zone-specific rules.
- Approved master record: Identification of the governing sample and revision status.
- Limit-sample register: Photo and sample list for acceptable and non-acceptable borderline conditions.
- Revision history: Changes to tooling, finish route, artwork, construction, or packaging.
This package is useful because it reduces dependence on memory and email fragments. It also helps procurement, engineering, factory QA, and third-party inspectors work to the same standard. In cross-border trophy development, documentation discipline is often what protects consistency when teams are not in the same room.
Conclusion
Premium trophy appearance standards work best when buyers and manufacturers define cosmetic zones, inspection conditions, defect categories, and approved references before production starts. The right framework recognizes that not every surface can or should be judged the same way. Hero zones, reflective finishes, paint systems, engraved elements, and assembly joints each need practical rules linked to how the award is actually viewed and used.
There is no universal premium trophy quality standard that fits every design. Exact defect limits, sample counts, and acceptance thresholds must be aligned to the project, documented clearly, and confirmed through approved samples. As a custom trophy manufacturer and project partner, Me Trophy can support drawing review, zone mapping, sampling strategy, casting, plating, polishing, painting, assembly, and appearance planning for OEM and ODM programs, with company-specific workflow details requiring confirmation for the project. For teams that want deeper process-assurance guidance alongside appearance criteria, review Me Trophy’s quality control resources.
FAQs
1. What is the best way to define trophy cosmetic zones?
The best method is a zone drawing that labels hero, secondary, hidden, and contact areas on each SKU. It should include front, side, top, and detail views so both buyer and manufacturer can apply different appearance rules to different surfaces.
2. Should the same scratch standard apply to every part of a premium trophy?
No. A mirror-plated hero face usually needs a stricter trophy scratch defect limit than recessed cast textures, underside areas, or contact surfaces. Acceptance should be based on zone, finish, and agreed inspection conditions.
3. Why do buyers and factories disagree on plating cosmetic acceptance?
Disagreements often happen because viewing distance, lighting, orientation, and substrate expectations were never standardized. Reflective plating highlights imperfections differently under different inspection conditions, so those conditions must be agreed before approval.
4. What samples should govern premium trophy appearance approval?
A complete package should include a golden sample, approved master, retain samples, and limit samples for borderline conditions. This gives all parties a physical reference for finish, color, plating tone, engraving appearance, and assembly alignment.
5. How can reorder consistency be controlled for custom trophy programs?
Use the same approved master, cosmetic-zone drawing, appearance specification sheet, and limit-sample register for replenishment orders. Any change to tooling, polishing, plating source, paint system, or packaging should trigger review against the approved standard.