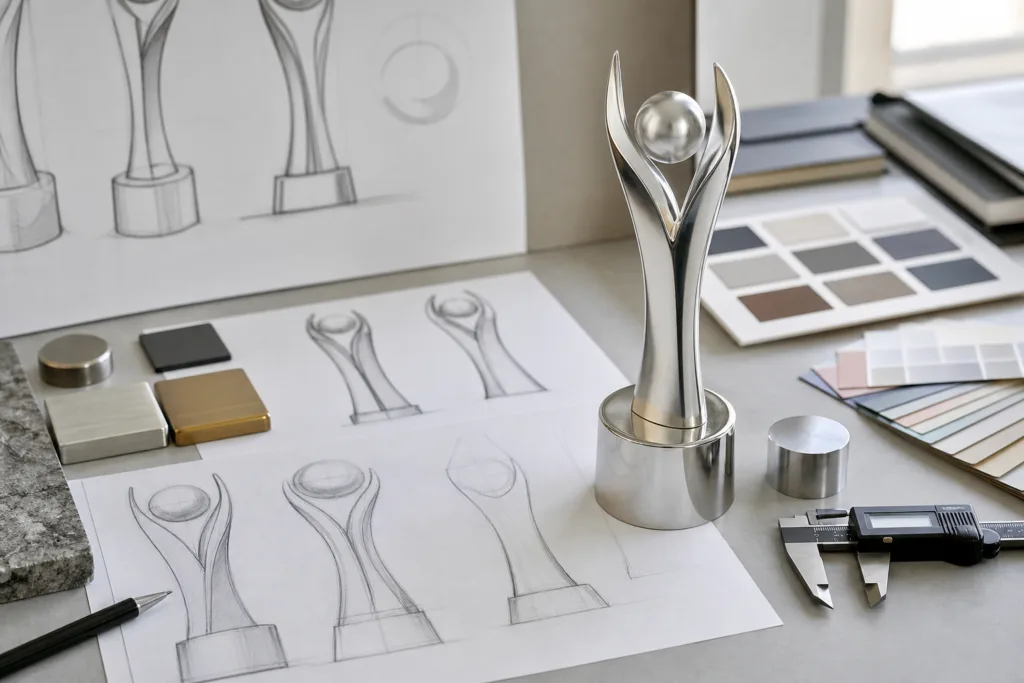
For branded awards, Pantone trophy color matching is not just a design preference. It is a production-control topic that starts with artwork and specifications, then continues through substrate preparation, paint selection, sampling, approval, inspection, and repeat-order recordkeeping. When sourcing painted metal trophies, buyers should treat color as a managed process rather than assuming a Pantone code alone will guarantee the final result on a metal surface.
That distinction matters because painted coatings behave differently on zinc alloy, copper, and other metal trophy components than ink on paper or color on a screen. Geometry, polishing condition, primer build, sheen, and lighting all change how the same reference appears. For brand managers, designers, and quality teams, the practical goal is to convert internal brand standards into a production-ready brief, then approve a physical sample that defines what is acceptable for bulk production and repeat orders.
For international OEM and ODM trophy projects, Me Trophy can support painted-finish development as a manufacturing partner by helping buyers translate visual intent into manufacturable specifications, sampling steps, and inspection checkpoints. Project-specific tolerances, paint systems, and repeat-order controls should still be confirmed for the program.
Translate Brand Color Standards Into a Production Brief
The first step in a custom trophy Pantone color project is turning brand guidance into a manufacturing brief that can be used by design, procurement, sampling, and production teams. Many color issues begin because the buyer sends only a logo file and a Pantone number, while the factory still lacks the information needed to judge feasibility, masking areas, finish interaction, and approval criteria.
A stronger brief should define the intended color application in practical terms:
- Pantone system reference: specify the exact Pantone code and the guide context the brand team uses, and confirm whether that reference is being used as a target appearance rather than a guaranteed ready-made coating.
- Target paint area: identify which parts of the trophy require the color, such as the emblem, figure, shield, base trim, inset panel, or full body.
- Base material: state whether the colored area is on zinc alloy, copper, steel, aluminum, resin insert, or another component, because substrate affects preparation and appearance.
- Finish expectation: clarify gloss, matte, satin, metallic, or textured appearance.
- Brand hierarchy: note which branded area is most critical if multiple colors or finishes are involved.
- Artwork package: include vector artwork, color callouts, dimensioned layout, and part-by-part finish mapping. Buyers preparing new developments may find Me Trophy’s guidance on artwork and CAD requirements useful for reducing interpretation risk.
- Approval chain: define who reviews digital renderings, pre-production samples, and final color approvals on the buyer side.
One common procurement question is: Which Pantone system and sheen apply? In practice, the answer should be written into the RFQ or development brief at the beginning. A brand may carry one Pantone code in internal guidelines, but the trophy project still needs to identify the intended finish and physical reference standard used for comparison. If this is not defined early, sample review may become subjective, especially when a glossy curved metal surface is compared with a flat printed guide.
Pantone’s own support documentation notes that Pantone colors for paint are matched using Pantone guides or chips to create the closest available paint match, which is why a physical approval step remains important for coated products rather than assuming the code alone controls the outcome. See https://support.pantone.com/en/how-do-i-get-paint-in-a-pantone-color.
In B2B trophy manufacturing, the practical rule is simple: define the color target, define where it applies, define how it should look, and define who has the authority to approve it. Final production feasibility, exact coating recipe, and any project-specific color control method should be confirmed with the manufacturer.
Understand Substrate, Primer, and Sheen Effects
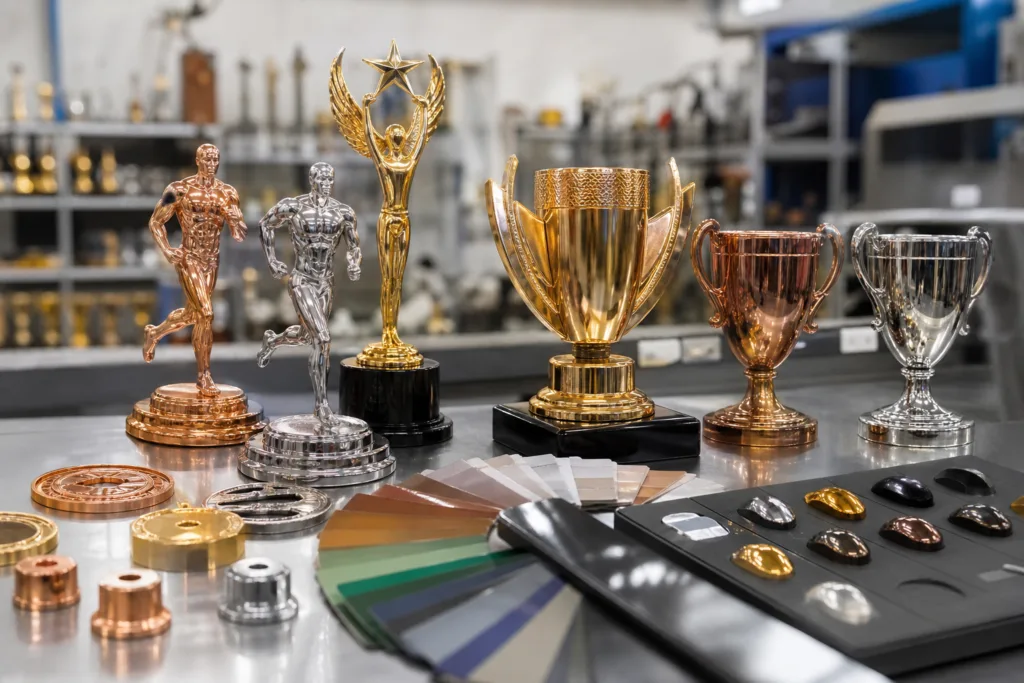
Buyers often assume the paint itself determines the final appearance. In fact, the substrate and preparation system can change the visual result significantly. For a metal award, the same nominal color may appear deeper, lighter, warmer, cooler, or more reflective depending on what is underneath it and how the part was prepared.
Several manufacturing variables matter:
- Substrate type: zinc alloy and copper can accept painted finishes, but casting density, porosity, and local surface condition can influence primer behavior and topcoat appearance.
- Die-cast geometry: sharp recesses, raised logos, textured zones, and narrow edges can affect paint build and visual uniformity.
- Primer build: primer thickness, hiding power, and smoothness influence the final topcoat tone and consistency.
- Edge radii: very sharp edges can show thinner paint or weaker coverage compared with flat central surfaces.
- Polishing condition: a highly smoothed metal surface and a less refined surface may receive topcoat differently, especially with semi-gloss or metallic systems.
- Surface preparation: cleaning, sanding, blasting, or other preparation methods influence adhesion and the look of the final coating.
This is why painted-finish development should not be separated from manufacturing reality. A buyer may approve a flat color chip, yet the same hue on a curved medal top, a die-cast cup body, or an inset logo panel can look different after primer and topcoat are applied.
Sheen is equally important. Gloss surfaces tend to reflect more light and may look more saturated or darker at certain angles. Matte finishes scatter light and can make a color appear softer. Satin finishes often land between those two visual effects. Metallic and textured coatings introduce additional visual movement, which means they should not be evaluated as if they were flat solid colors.
When planning spray painted trophy finish options, buyers should discuss available paint and color finishes in relation to the chosen base material and part geometry. A finish that works well on one award style may need adjustment on another because the shape and surface condition are different.
The key procurement point is that painted trophy color tolerance is not just about a color formula. It depends on substrate, primer, topcoat, sheen, and the visual standard used for approval. Exact tolerance capability and production controls must be confirmed for the project rather than assumed from a digital mockup.
Select Pantone References and Physical Masters
Once the project brief is clear, the next step is choosing the reference standard that production and inspection will use. This is where many teams reduce future disputes by separating three different things: the brand reference, the manufacturing target, and the approved production master.
Best practice is to define the Pantone reference in writing and then create a physical comparison path for the trophy finish. The brand reference may come from a design guide. The manufacturing target may be a matched coating trial. The approved production master is usually the signed sample that both parties use for later comparison.
A useful approval structure includes:
- Brand reference: the designated Pantone code or physical chip identified by the buyer.
- Trial panel or component sample: an initial metal award paint sample showing how the color behaves on the intended substrate and finish system.
- Approved trophy sample: a completed or representative part signed off as the standard for bulk production.
- Retained control sample: a protected reference held for later lot comparison and repeat-order continuity.
This stage is where Me Trophy’s sample production capability becomes commercially important. For painted awards, the sample is not just for aesthetic review. It is the checkpoint where the buyer verifies color, sheen, masking lines, edge coverage, and the combined effect of substrate plus coating.
A critical procurement question is: Who has final authority when physical and digital references differ? The safest answer is to define precedence in writing before sampling starts. In many B2B programs, a signed physical sample takes precedence over screen images or uncalibrated digital proofs because the manufactured coating is what bulk production must follow. If the buyer wants the Pantone chip to remain the primary standard, that should also be written clearly, together with the acceptable interpretation method on metal.
Do not leave this decision informal. If the approval hierarchy is unclear, repeat orders may drift because one team uses artwork files as the main standard while another uses prior bulk pieces or memory-based visual judgment.
For measurable color control, some projects may also consider instrumental methods. ASTM guidance supports defining color tolerances instrumentally for painted parts, while also recognizing that gloss, texture, and viewing conditions affect commercial acceptability. See https://store.astm.org/standards/d2244. Any numerical threshold, instrument setup, or pass-fail rule for trophies should be confirmed specifically for the project.
Review Samples Under Consistent Lighting
Color decisions made under inconsistent lighting are one of the fastest ways to create avoidable disputes. A trophy sample reviewed under warm office lighting may not look the same under daylight, retail spotlights, or event venue conditions. That does not mean the coating is wrong; it means the review method was not controlled.
Sample review should therefore use agreed viewing conditions as much as possible. Even if a buyer and manufacturer are in different countries, they can still align on the review method and document it in the approval record.
Recommended review controls include:
- Lighting type: define the preferred viewing condition for approval and note any secondary lighting conditions relevant to the event or display environment.
- Background: use a neutral, non-distracting background to reduce color contamination from surrounding surfaces.
- Viewing distance: define the normal inspection distance for overall appearance and a closer distance for defect review.
- Viewing angle: examine flat and curved areas from consistent angles because gloss and metallic effects change with movement.
- Part orientation: keep the sample in a repeatable position when comparing multiple pieces.
- Reference presence: compare the sample against the designated physical standard, not memory alone.
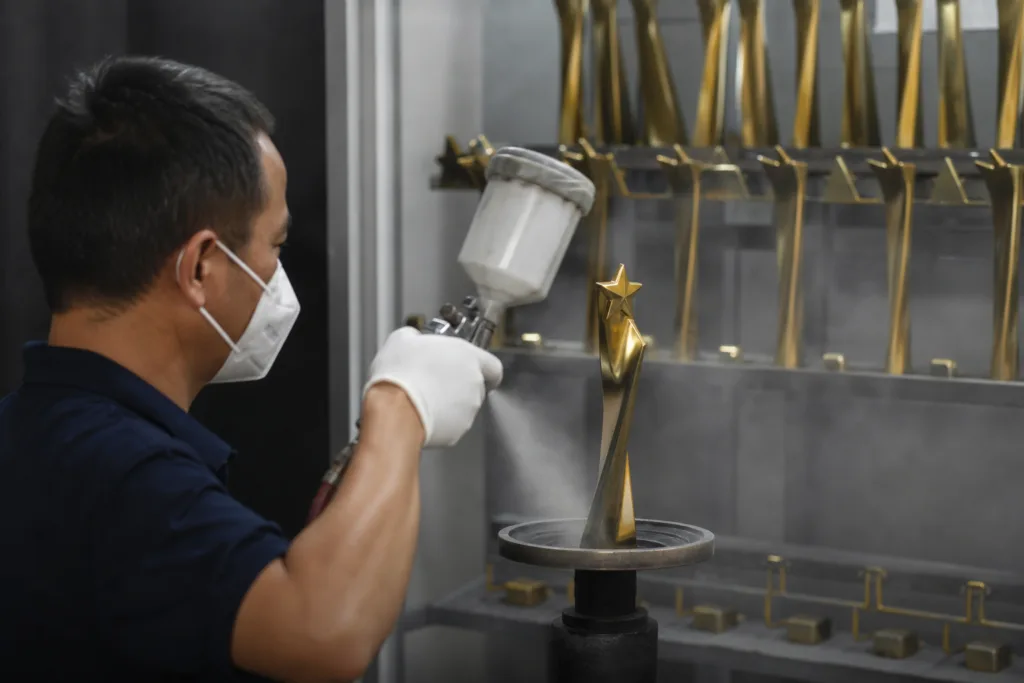
For complex painted awards, it is wise to evaluate the finish after the manufacturer’s spray painting process under agreed conditions before giving final color approval. This helps buyers confirm not only the hue but also the practical look of the cured coating on edges, recesses, and visible presentation surfaces.
A simple but effective tool is a color-approval form paired with a controlled viewing checklist. That document can record the project code, Pantone target, finish description, sample date, reviewers, lighting condition, observations, revision history, and final sign-off. For sourcing teams managing multiple trophy programs, this creates traceable decisions instead of relying on email screenshots and verbal comments.
If multiple stakeholders must review the sample, assign one final approver. Otherwise, designers may comment on brand appearance, procurement may focus on consistency, and quality teams may focus on defect limits, yet no one formally decides which revision is accepted for production.
Define Acceptable Range and Defect Boundaries
After a sample is approved, the next question is not whether every unit will look identical under all conditions. The practical question is what variation is acceptable for the project. This is where buyers and manufacturers should align on visual standards and inspection boundaries before mass production begins.
For painted trophies, acceptable range should cover both color and finish condition. Typical review points include:
- Overall color variation: how closely production pieces should match the approved sample under agreed viewing conditions.
- Batch-to-batch shift: what level of lot variation is acceptable on repeat runs.
- Edge coverage: whether slight thinness on sharp edges is acceptable or not.
- Orange peel: what surface texture is acceptable for the selected sheen.
- Dust points and particles: how many, where, and at what size they become rejectable.
- Pinholes or voids: whether they are allowed in hidden areas, visible faces, or not at all.
- Thin paint and show-through: where substrate visibility or poor hiding is unacceptable.
- Overspray and masking lines: the standard for clean separation between painted and unpainted areas.
- Gloss inconsistency: whether local sheen change is allowed on curved or recessed areas.
From a quality-management standpoint, painted trophy color tolerance should be defined as a mutually agreed quality standard tied to the approved sample and the inspection method. The most effective approach is to combine a retained physical standard with a written defect checklist and, if required, an agreed measurement method.
Me Trophy’s quality control approach can support this kind of structured review, but the exact numerical tolerances, instrument methods, inspection sampling plan, and reject thresholds must be confirmed for the specific order.
Buyers should also distinguish between critical defects, major defects, and minor cosmetic variation. A visible color mismatch on the front logo plate may be critical for a branded championship award, while a slight texture change on a hidden underside may be acceptable. Writing these priorities into the specification prevents the inspection team from overreacting to low-risk areas while missing what the brand team actually cares about.
In short, do not approve only a color. Approve an appearance standard with boundaries.
Preserve Color Records for Repeat Orders
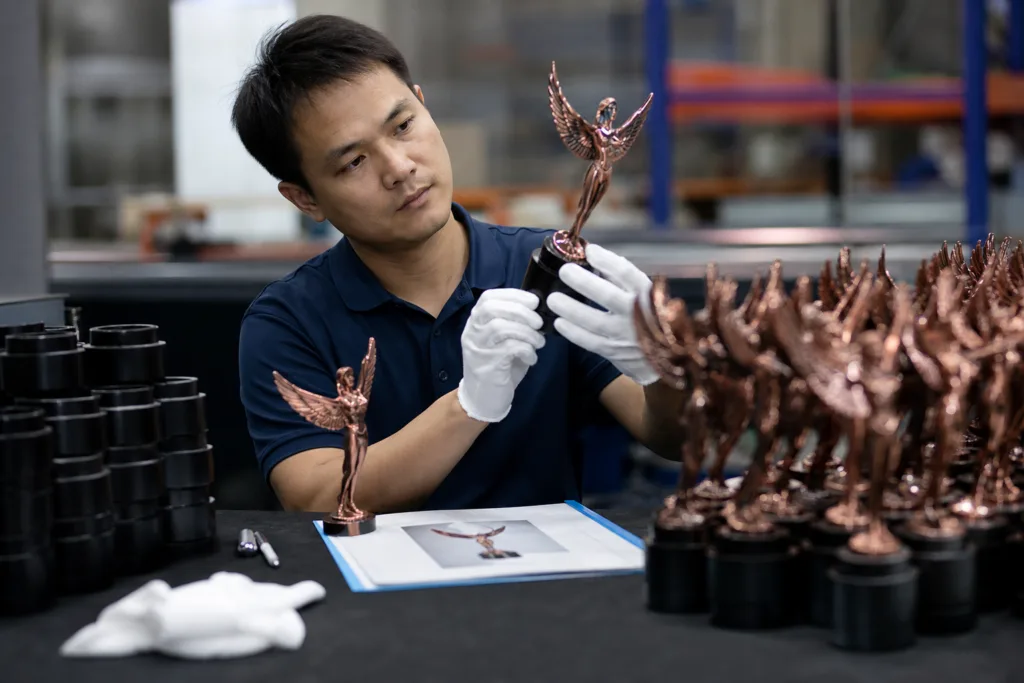
Repeatability depends less on memory and more on documentation. Once a project reaches approved production, buyers should archive the records that make future reorders more stable. This matters especially for annual sports events, recurring corporate recognition programs, and distributor-led private-label award lines where the same visual identity must carry across different order dates and delivery batches.
Useful records include:
- Approved physical sample: signed and dated, with storage conditions that protect the finish from fading or damage.
- Retained control sample: held by the manufacturer for production comparison.
- Pantone and finish specification: including sheen description and any agreed visual notes.
- Paint code or supplier reference: if available for the project and approved for recordkeeping.
- Primer and process notes: enough detail to support consistent re-development, subject to what the manufacturer confirms it can retain and disclose.
- Inspection photos: especially of key visual areas and edge conditions.
- Approved defect criteria: documented acceptance boundaries.
- Revision history: what changed from sample round to sample round and which version was signed off.
This record set supports future OEM and ODM programs because it reduces reliance on staff memory, changing email threads, or old artwork folders with unclear status. It also helps reduce color drift across wholesale and export deliveries, where different production windows, coating batches, or logistics schedules can introduce variation if no master reference is preserved.
When planning repeat customization programs for painted metal trophies, buyers should ask the manufacturing partner how approval samples, finish references, and project records are archived for later production continuity. Exact retention practices and repeat-order matching controls should be confirmed directly for the program.
The commercial value of this discipline is simple: fewer approval disputes, faster reorder alignment, and a better chance of maintaining brand consistency when the same award family is produced over time.
Related Reading
- painted vs electroplated trophies
- trophy materials and finishes
- inspection checklist for bulk orders
- custom trophy RFQ guide
- technical documents
Conclusion
Controlling brand color on painted awards requires a chain of decisions, not a single Pantone code. Buyers should begin with a clear production brief, confirm the target finish and substrate context, select the right physical references, review samples under consistent lighting, define acceptable variation and defect boundaries, and preserve records for repeat orders.
For international B2B projects, Me Trophy can work as a manufacturing partner to translate brand color intent into production-ready painted trophy specifications, sample approvals, and repeat-order reference management. That said, final tolerances, approval criteria, paint-system details, and inspection methods should be confirmed for each project before bulk production starts.
Frequently Asked Questions
1. Does a Pantone code guarantee the same color on a painted metal trophy?
No. A Pantone code is a target reference, but the final appearance on metal depends on substrate, primer, topcoat, sheen, geometry, and lighting. That is why a physical sample approval step is recommended for painted trophy projects.
2. What should buyers include in a custom trophy Pantone color brief?
At minimum, include the exact Pantone reference, intended sheen, paint location, base material, artwork files, finish mapping, visible priority areas, and the buyer-side approval chain. If digital and physical references may conflict, define which one has final precedence.
3. Why can the same color look different on gloss and matte trophy finishes?
Gloss reflects light more directly, while matte scatters light. This changes perceived depth, saturation, and brightness even when the nominal color target is the same. Metallic and textured finishes can change perception even more.
4. How should a metal award paint sample be approved?
It should be reviewed under agreed lighting, against the designated physical reference, with notes covering hue, sheen, coverage, masking quality, and visible defects. A signed approval sample and retained control sample are useful for bulk production and repeat orders.
5. Can painted trophy color tolerance be defined numerically?
It can be, but the method must be agreed for the project. Some programs use instrumental color difference methods together with visual approval, while others rely primarily on signed samples. Numerical limits, measurement setup, and reject thresholds should be confirmed with the manufacturer.