Cosmetic plating defects on awards can affect more than appearance. For procurement teams, inspectors, and finish engineers, a visible surface issue can change lot acceptance, trigger replacement risk, delay event deadlines, and create disputes over whether the problem is isolated or systemic. This guide is built for buyers reviewing electroplated trophies and metal awards where finish quality matters as much as structural fit and branding accuracy.
The goal is practical classification, not guesswork. When an inspector sees pitting, blistering, burns, stains, bare areas, or color mismatch, the first task is to document observable evidence under controlled conditions. Buyers then need to ask two commercial questions: is the issue limited to a few parts or spread across the lot, and which approved sample or appearance standard governs acceptance? Those questions matter because ad hoc judgment often leads to inconsistent decisions between sourcing teams, factories, and end customers.
For custom trophy programs, Me Trophy can support finish expectation setting, sampling review, and manufacturing discussion as an OEM/ODM project partner. Any company-specific process capability, acceptance protocol, or lead-time commitment should be confirmed for the project.
Create Controlled Lighting and Cosmetic-Zone Conditions
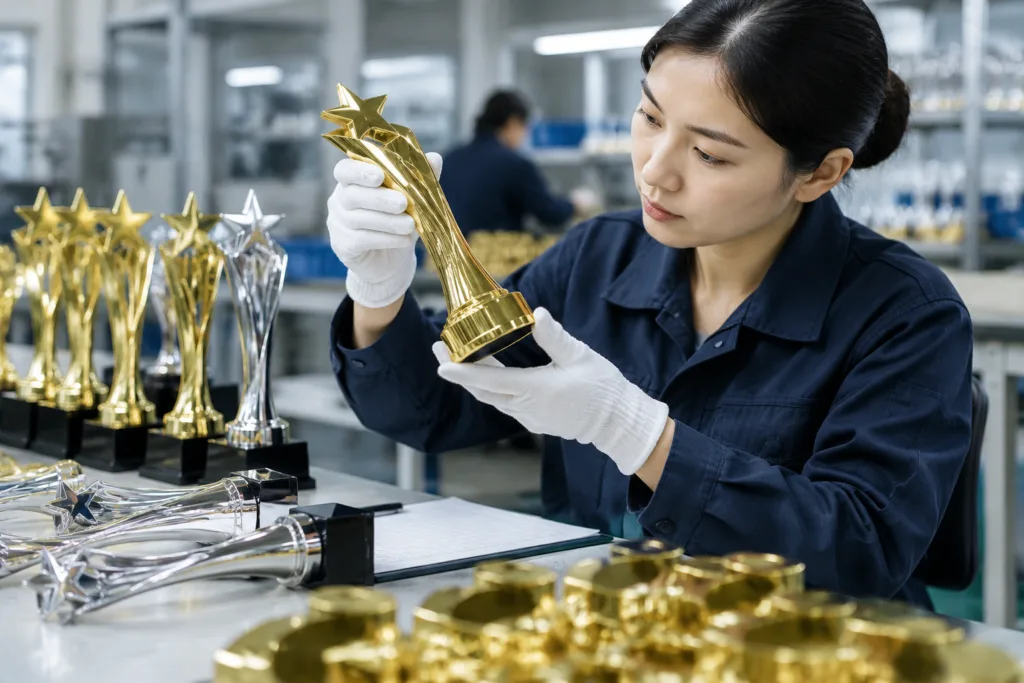
Before judging any electroplating defects trophy inspectors must first stabilize the inspection environment. Decorative plating is highly reflective, so the same part can appear acceptable or defective depending on light angle, handling marks, and viewing position. A repeatable setup reduces disagreement and helps teams compare like with like.
Start with consistent lighting direction and intensity. Use a neutral background, avoid mixed light sources, and keep the part clean before inspection. Fingerprints, dust, and packaging residue can mimic stains or color shift. Viewing distance and angle should be agreed in advance, especially for presentation surfaces that will be seen at arm’s length. ASTM guidance also supports evaluating appearance under controlled and comparable reflected-light conditions rather than informal shop-floor viewing: https://store.astm.org/d3964-10r25.html.
Part orientation also matters. If one inspector checks a cup upright and another tilts it toward the light, the same zone can look different. Use a fixed orientation for fronts, sides, top surfaces, and assembly transitions. Then define cosmetic zones clearly:
- Primary cosmetic zones: front-facing cup walls, figurines, medallion faces, prominent logos, and visible trim rings.
- Secondary cosmetic zones: side walls, rear faces visible in normal handling, and upper stem transitions.
- Low-visibility zones: hidden joints, undersides, internal recesses not seen in normal display, and concealed mounting interfaces.
On metal awards, visibility is not uniform. Recessed logos may tolerate minor texture differently from a mirror-polished front panel. A sharp edge on a die-cast emblem may reflect more strongly than a broad flat surface and therefore reveal minor finish variation more clearly. Inspect the same area under identical conditions across all samples.
When available, a signed appearance standard, approved master sample, or buyer-approved retain sample should govern evaluation. If none exists, note the increased acceptance risk in the inspection report. This is especially important when the order includes multiple finishes from the same family of electroplating finish options, because verbal descriptions such as bright gold or antique silver do not fully define acceptable color and sheen.
Identify Pits, Blisters, Burns, Stains, and Bare Areas
A useful trophy finish defect inspection system depends on shared definitions. The purpose is not to prove root cause on the spot, but to describe what is visible so the manufacturer and buyer can make a consistent decision.
Pits
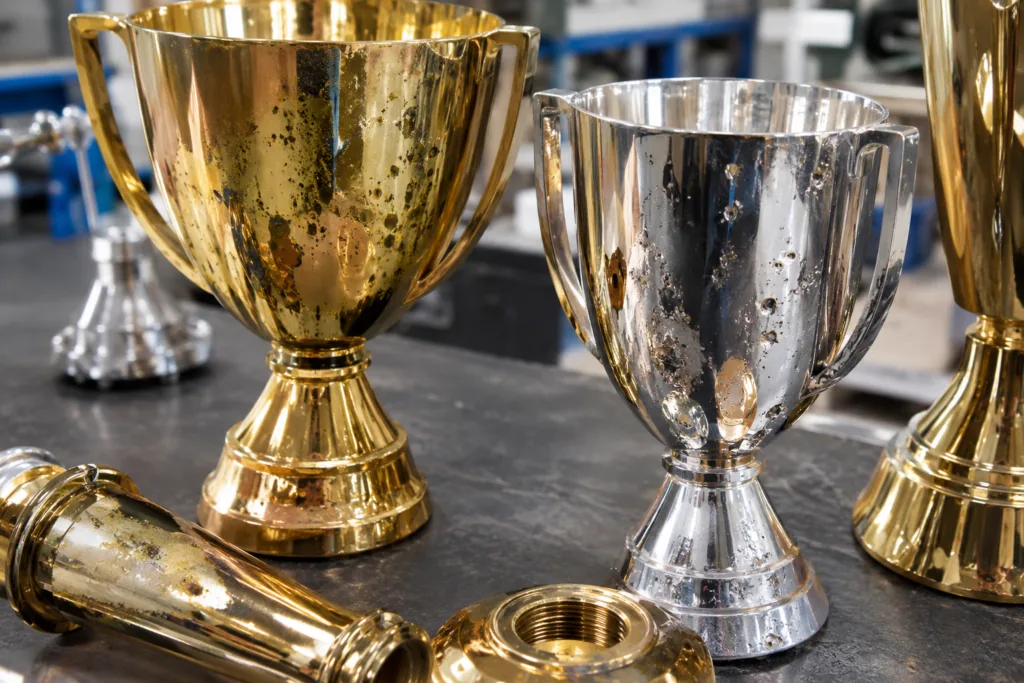
Pits are small depressions, pinhole-like interruptions, or crater features that break the continuity of the plated surface. In reflective finishes, even tiny pits can disrupt image clarity and highlight distortion. Record pit size, count per part, whether pits are isolated or clustered, and whether they sit in a primary cosmetic zone. Also note if the defect appears as a true depression or if it seems related to underlying porosity.
Blisters
A plating blister metal award defect appears as a raised bubble, dome, or local lifting area. Some blisters are obvious domes; others show slight edge lifting that becomes visible only when the light is moved. Inspectors should record appearance evidence first: shape, diameter, location, whether the surface can be pressed or cracked, and whether multiple parts show the same pattern. Avoid premature statements about adhesion failure unless supported by the agreed inspection or test plan.
Burns
Burns often appear as over-bright, rough, darkened, or uneven zones, commonly near edges, points, or other high-current areas. On trophies, these may concentrate on sharp figurine contours, raised lettering, thin trim sections, or corners near hanging geometry during the electroplating process. Record whether the area is rough to the eye, visually over-developed, darker than adjacent surfaces, or irregular in reflectivity.
Stains and discoloration
These include localized patches, streaks, fingerprints, water marks, rainbowing, residue, or chemical-looking films. Some are true finish issues; others may come from post-plating handling or packaging. Record color tone, shape, wipeability if checked under the agreed procedure, and whether marks are random or repeat at the same location across parts.
Bare areas
Bare areas show exposed substrate, thinly covered zones, or obviously incomplete coverage. On a bright decorative surface, they may appear dull, dark, or of a different base-metal color. Document whether the exposed area is on a sharp edge, recess, inside corner, threaded point, or assembly interface. Coverage issues in hidden areas may be classified differently from visible faces, but they still need recording.
For every defect type, record the same core evidence:
- Defect type and visible characteristics
- Approximate size or dimensional range
- Count per part and whether clustered
- Cosmetic zone and visibility at agreed viewing distance
- Effect on reflectivity, gloss, or image clarity
- Whether found on one part, one subgroup, or multiple parts in the same lot
Distinguish Substrate Defects From Plating Defects
Not every appearance issue is created by the plating layer itself. Metal award components made from die-cast zinc alloy, copper, or related decorative metals can carry pre-existing conditions that become more visible after finishing. Classification accuracy matters because containment and corrective action differ depending on whether the issue began in casting, machining, polishing, assembly preparation, or plating.
Common substrate-related conditions include porosity, pinholes from cast structure, sink marks, mold-line witness, sanding scratches, polishing waves, edge thinning, and uneven surface geometry. Decorative plating can amplify these features rather than create them. For example, a polishing ripple may read as uneven sheen after plating, while a casting pore may later appear as trophy plating pitting.
Use this evidence checklist before assigning the defect category:
- Compare the defect shape to the underlying geometry. Does it follow a mold line, corner radius, or polishing direction?
- Inspect edges and recessed features. Sharp edges may reveal exposure or thin coverage that originates from geometry sensitivity rather than random plating failure.
- Review pre-plating photos or in-process samples if available. A pre-existing pit or wave can often be seen before final finish.
- Check repeatability. Does the same pattern recur on parts from one cavity, one tool area, or one polishing station?
- Look for surface-preparation clues such as directional scratches or buffing distortion associated with surface preparation.
The key point is discipline. If the evidence suggests an underlying substrate feature telegraphing through the finish, record that classification as provisional and request manufacturing trace-back. If the issue appears only after plating and not in pre-finish evidence, document that too. The purpose is to support containment and supplier discussion, not to make unsupported fault claims during incoming inspection.
Assess Color and Sheen Variation Across Parts
Electroplated trophy color variation is one of the most common causes of buyer disagreement because it is highly visible but not always easy to define. A lot can contain acceptable minor part-to-part change, or it can include obvious mismatch that breaks set consistency. The difference depends on the approved reference and the viewing method.
Inspect color and sheen in a structured sequence. First compare front-facing primary surfaces against the approved reference. Then compare similar parts side by side within the lot. Finally inspect assembled combinations such as figurine, emblem, stem, trim ring, and base cap together, because mismatch often becomes more obvious after assembly than when each item is viewed alone.
Record the type of variation observed:
- Hue difference: one part reads redder, yellower, bluer, or greyer than another.
- Lightness or darkness shift: the finish looks lighter, deeper, or more muted.
- Gloss mismatch: one surface appears brighter or flatter than the reference.
- Haze: reduced clarity or milky appearance over a reflective finish.
- Patchiness: uneven color distribution across one surface.
- Rainbowing or iridescent film: localized interference-like color cast.
- Directional sheen variation: a surface looks different when rotated because texture or polish direction changes reflectivity.
Acceptance should be tied to an approved sample and to a clearly defined evaluation method. That method may be visual, instrument-based, or both. If no agreed standard exists, state that acceptance risk rises and a project review is needed before mass production continues. BYK’s appearance resource is useful when discussing objective evaluation of gloss, haze, and related visual properties: https://www.byk-instruments.com/appearance.
Also check for non-process influences. Protective film residue, tissue rub, carton abrasion, and glove or hand marks can mimic electroplated trophy color variation. Before labeling the issue systemic, confirm whether packaging or assembly handling introduced visible marks after finishing. This is why buyers should align finish expectations with approved retain samples before release to mass production, not after goods are packed.
Record Defect Location, Frequency, and Severity
Inspection only becomes actionable when observations are structured into data. For plating quality control trophy projects, a report should allow engineering, sourcing, and factory teams to understand what happened, where it occurred, how often it appeared, and how visible it was.
At minimum, record:
- Part number or component description
- Lot or batch identifier
- Finish or color name used for the project
- Inspection date and inspector name
- Cosmetic zone classification
- Defect type
- Exact location on the part
- Quantity per part
- Percentage of affected parts in the sample or lot
- Severity based on visibility under agreed conditions
Marked photos are highly effective. Use circles, arrows, and orientation labels such as front, top, left side, or emblem recess. A simple defect map can show whether problems cluster on edges, recessed logos, stem joints, or one side of a figurine. This helps distinguish isolated damage from recurring pattern issues.
An acceptance matrix tied to the approved appearance reference can simplify decisions. For example, the matrix may classify defects by zone and visibility instead of relying on broad pass or fail language. Lot-level analysis then shows whether the issue is random, feature-specific, or systemic across production. ASTM B602 provides context for structured sampling of metallic coatings when formal lot-based inspection is needed: https://store.astm.org/b0602-88r16.html.
International projects benefit from bilingual or image-led reports. When teams in different regions are reviewing the same trophy finish defect inspection findings, labeled photos and a concise defect code system reduce translation errors. Me Trophy can support project communication and quality control alignment, with any specific acceptance methods or inspection plans requiring confirmation for the program.
Use Findings for Containment and Corrective Action
Once defects are classified, the next step is containment. Avoid jumping directly to technical conclusions. First identify scope. Segregate affected lots and ask whether the issue is limited to one finish color, one component, one mold cavity, one rack position, one production date, or one packaging batch.
Containment questions should include:
- Are nonconformities concentrated in one cosmetic zone or spread across the whole part?
- Do affected parts share one geometry, one cavity, or one assembly interface?
- Is the issue visible before assembly, after assembly, or only after packing?
- Does the same defect recur in one finish only or across multiple finishes?
- Are replacement parts matching the approved reference or only the rejected lot average?
Then move to corrective-action questions for the manufacturer or plating partner:
- What approved sample governs color, brightness, and cosmetic acceptance?
- Did the issue occur on all parts or only on specific geometries?
- Are defects concentrated in recessed areas, sharp edges, or high-visibility surfaces?
- Is there evidence from pre-plating polishing or substrate review that explains the pattern?
- Could assembly, base fitting, protective wrapping, or carton movement have introduced rub marks or stains after plating?
For custom awards, these questions often cross department boundaries. A color mismatch on a figurine may be connected to a different production date than the stem. A bare edge at a trim ring may involve base fit, polishing approach, or local geometry. A blister on a medallion face may require review of incoming substrate condition, handling history, and finish route together.
As a manufacturing partner, Me Trophy can support project review, sample alignment, custom-base and assembly interface review, and prevention-focused discussion. When a project needs deeper review of finish expectations or a new sample approval path, buyers can request a project review. Any company-specific controls, acceptance standards, or prevention measures must be confirmed for the order.
Recommended Inspection Assets and Workflow
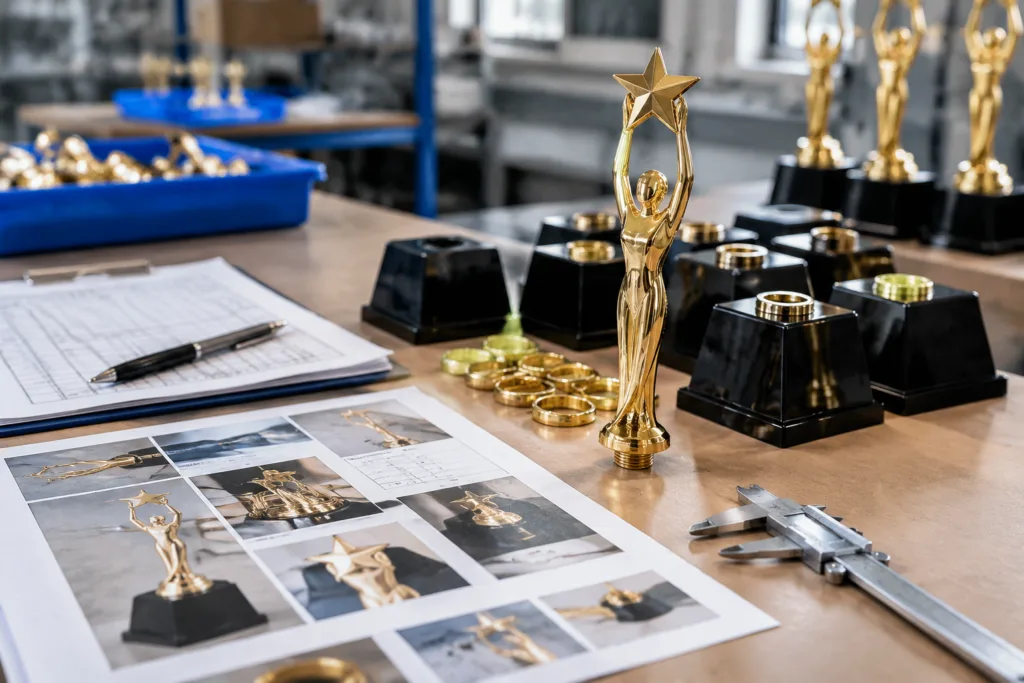
Two practical tools can improve repeatability across repeat orders, OEM/ODM development, and export quality coordination.
1. Defect taxonomy photo board
This visual board should show accepted versus rejected examples of pitting, blistering, burns, stains, bare areas, and color variation under the same lighting, orientation, and cosmetic-zone rules. The goal is not artistic presentation. It is calibration. Teams should be able to point to a photo and say this condition matches category A in zone 1, or this condition exceeds the approved sample.
Good photo boards include:
- Part name and finish identification
- Zone labels
- Accepted and rejected examples for each defect type
- Close-up and normal-view images
- Reference to the governing sample or sign-off date
2. Inspection record template
The record template should support lot-level trend analysis, supplier communication, and future repeatability. It should be simple enough for inspectors to use consistently and detailed enough for engineers to diagnose patterns later. Include fields for batch, part orientation, defect map, photo number, severity, provisional classification, and disposition decision.
Keep both tools with sample approvals and finish expectation documents. This helps when reordering the same championship series, launching a new branded award, or comparing a new production run to a prior approved lot. It also reduces disputes when appearance memory differs between buyer and factory months later.
Conclusion
Accurate assessment of electroplating defects trophy programs depends on four disciplines: controlled inspection conditions, precise defect classification, clear separation of substrate versus plating-layer issues, and strong documentation. Pitting, blistering, burns, stains, bare areas, and color mismatch should be judged by visible evidence, not by assumptions made under inconsistent lighting or without a governing sample.
For buyers, two questions should stay at the center of every review: is the issue isolated or systemic, and which approved reference sample governs appearance acceptance? When those questions are answered with documented evidence, sourcing and manufacturing teams can make faster decisions on containment, replacement, and corrective action.
If your team is defining finish expectations for electroplated trophies, reviewing sample approvals, or troubleshooting a current lot, Me Trophy can support sampling alignment and prevention-focused manufacturing discussion as an OEM/ODM project partner. For related references, see the list below and submit an inquiry when a custom project needs appearance-standard alignment or production review.
- bulk inspection checklist
- electroplating vs painted trophies
- copper vs copper-plated trophy
- sample review process
- technical documents
FAQs
1. How should inspectors check trophy plating pitting consistently?
Use controlled lighting, a neutral background, fixed viewing distance, and an approved reference sample when available. Record pit size, count, clustering, cosmetic zone, and whether the depression disrupts reflectivity. Consistency matters more than informal spot checking under mixed light.
2. What is the difference between a plating blister metal award defect and a surface stain?
A blister is usually a raised bubble, dome, or local lifting feature, while a stain is a flat discoloration, patch, streak, or residue mark. Inspectors should document visible form and location first, then ask for manufacturing review rather than assume root cause from appearance alone.
3. How can buyers tell whether electroplated trophy color variation is acceptable?
Compare the lot to an approved master sample or signed appearance standard under repeatable viewing conditions. Review front-facing surfaces first, then side-by-side parts, then assembled components. If no approved standard exists, acceptance risk increases and project review is recommended.
4. Are all pits and rough areas caused by plating?
No. Some visible issues originate in the substrate, such as casting porosity, polishing waves, sanding scratches, or edge geometry that becomes more obvious after finishing. Inspectors should compare defect shape to part geometry and review pre-plating evidence when available.
5. What should a trophy finish defect inspection report include?
At minimum include part number, batch, finish name, date, cosmetic zone, defect type, exact location, count per part, percentage of affected parts, visibility-based severity, and marked photos. This allows sourcing, engineering, and factory teams to judge whether the issue is isolated, recurring, or systemic.