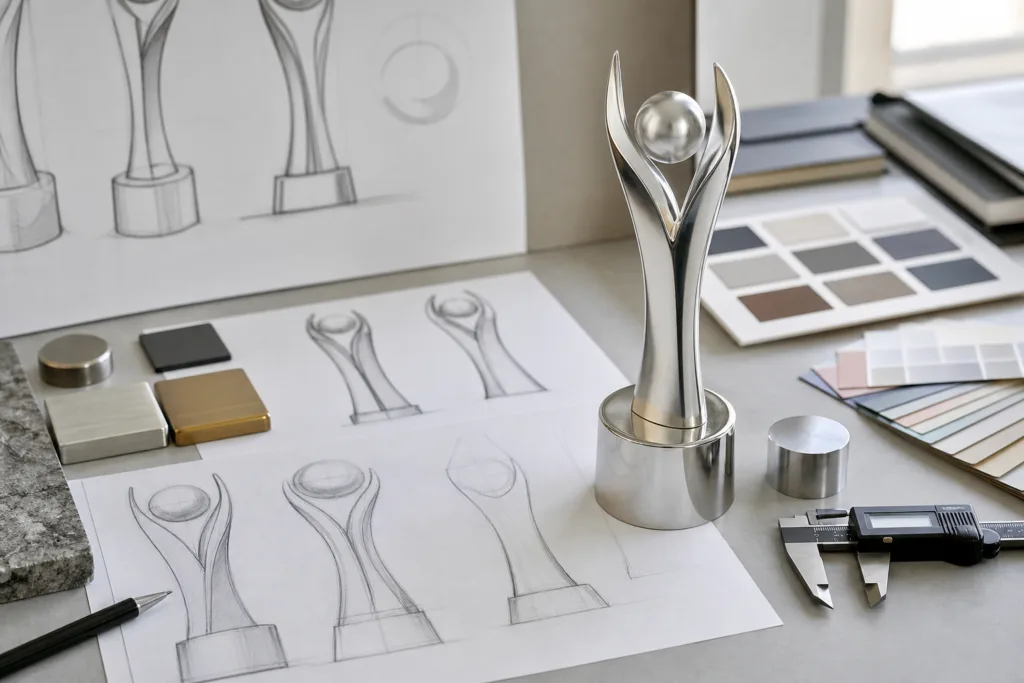
When a trophy concept includes mirror metal, satin contrast, antique recesses, and brand-color accents on one part, finish compatibility should be evaluated before tooling is finalized or samples are judged only by renderings. Many custom zinc alloy trophies can support plating, paint, and antique effects on the same casting, but the result depends on substrate quality, geometry, polish target, and process sequence. For procurement teams, the real question is not simply whether a finish is available. It is whether the chosen finish system is compatible with a zinc casting that can be manufactured, inspected, packed, and repeated in production. This guide includes a practical finish compatibility matrix and a sequencing diagram buyers can apply during RFQ review.
A zinc casting can often carry multiple finish zones, but only when visual boundaries are physically definable and each area can be prepared, polished, masked, plated, painted, or antiqued with repeatable control. That makes early collaboration between design, sourcing, and manufacturing especially important.
Start With Casting Surface and Design Intent
Finish decisions should begin with visual hierarchy, not with a list of decorative processes. Define what the viewer should notice first: a bright highlight, a satin field, an antique recess, a painted logo zone, or a color-filled emblem. If that hierarchy is unclear, tool design and sample review can drift toward surfaces that are technically possible but visually inconsistent with the original concept.
In practice, zinc alloy trophy finishes are constrained by the casting itself. Draft angles, textured fields, parting lines, gate-removal areas, sharp corners, deep recesses, and lettering depth all influence whether the intended finish can be achieved cleanly. A highly reflective plated surface will reveal subtle substrate issues. A painted recess may require deeper and more stable boundaries than a rendering suggests. Antique wiping needs enough recess definition to create contrast without looking muddy.
Can one casting carry multiple finish zones? In many cases, yes. However, manufacturability depends on whether boundaries are geometrically clear and whether technicians can access those zones for polishing, masking, plating, paint filling, or wiping without damaging adjacent areas. A raised border around a logo panel is usually more controllable than a vague visual transition across a broad curved face. Likewise, a recessed emblem with stable walls is easier to paint consistently than tiny isolated color islands scattered across textured metal.
During design review, identify primary viewing surfaces, frequent touch points, logo zones, and the exact boundary lines between finishes. This is where sourcing teams should ask practical questions: which side will be judged first in a presentation box, which edges are likely to be handled during award ceremonies, and which details must remain crisp after polishing and decorative treatment?
Base construction and integrated decorative elements should also be discussed early with Me Trophy when finish choices affect assembly, material transitions, or how the top component meets the base. If finish feasibility changes the underlying structure, buyers should align that discussion with the product architecture of custom zinc alloy trophies rather than treating decoration as a late-stage add-on.
Design review questions before tooling
- Which surfaces require bright reflection, and which can accept satin or antique texture?
- Where are the visible boundaries between metal and color?
- Are logo zones raised, recessed, or flush?
- Will the design expose parting lines or gate-removal areas in cosmetic faces?
- Can all finish boundaries be located consistently during production inspection?
Prepare Zinc Alloy for Cosmetic Finishing
Zinc casting surface preparation is the foundation of every cosmetic outcome. Before decorative finishing, the part may need trimming, deburring, defect review, filling if applicable, grinding, polishing, and cleaning. Me Trophy can align these steps with project intent, but the exact process route and acceptance thresholds should be confirmed for the project.
The relationship between polish level and final appearance is direct. Bright plating amplifies minor waviness, shallow scratches, and unstable edges because light reflects sharply from the surface. Satin looks can visually soften some variability, although they still require disciplined preparation. Antique effects rely on recess definition and wipe consistency; if recesses are too shallow or edges too soft, contrast may appear weak or irregular.
A plated zinc trophy and a painted zinc alloy award may begin with the same die casting, but preparation priorities differ. For plating, uniform smoothness, edge stability, and cosmetic metal continuity usually dominate. For paint accents or recess fill, boundary definition, recess geometry, and clean separation often become equally important. On mixed-finish projects, those priorities must be balanced together rather than optimized for only one decorative step.
Porosity, sink marks, cold shuts, rough texture, and unstable edges can affect adhesion, reflectivity, and line quality. NADCA die-casting standards note that design, production guidance, tolerances, and quality assurance for die castings influence the final surface available for decorative finishing, which is directly relevant when evaluating cosmetic zinc parts for plating and paint compatibility. See the industry reference here: https://www.diecasting.org/web/R_D/Standards/Die_Casting/Web/R_D/Die_Casting_Standards.aspx.
For buyers, the practical procurement task is to confirm what defect thresholds and cosmetic acceptance criteria the manufacturer can support for the project. Do not assume that a rendering-level surface can be achieved across every face of a complex casting without reviewing accessible polish zones, hidden areas, and likely visual priorities.
It is helpful to map the surface preparation process against each feature of the design. Raised rims, lettering, medal centers, sculptural figures, and back surfaces do not all respond the same way to grinding and polishing. A finish map should show where polishing access is easy, where it is restricted, and which surfaces are intentionally non-cosmetic.
Preparation notes for manufacturable finish zones
- Use recesses deep enough to support paint fill or antique wipe visibility.
- Avoid fragile knife-edge boundaries where metal finishing can soften the line.
- Keep text and logos large enough to retain clarity after polishing.
- Separate cosmetic and hidden areas clearly in drawings.
- Confirm whether local filling or correction is acceptable on non-primary surfaces.
Use Bright, Satin, and Antique Plating Effects
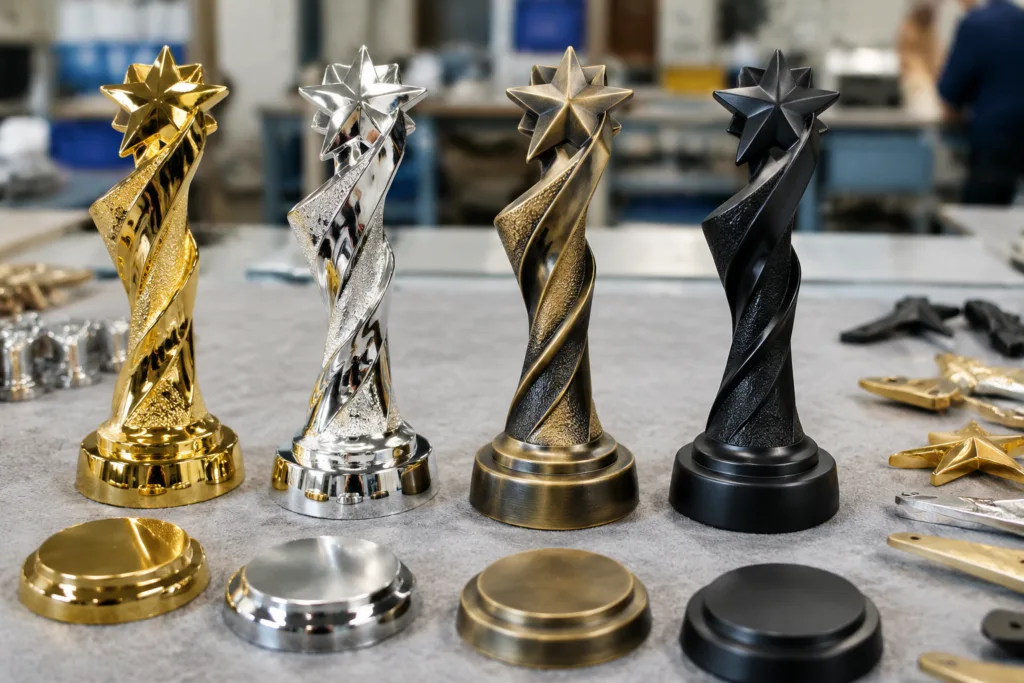
Common appearance goals for zinc trophies include bright reflective metal, satin or brushed-like visual contrast, and zinc trophy antique finish for added depth. Each effect depends not only on the decorative chemistry but also on the consistency of substrate preparation and any underlayers used in the plating system. Exact plating stacks, compatibility, and project-specific limits should be confirmed with the manufacturer rather than assumed from a color name alone.
Bright plating is usually most effective on broad, visible surfaces with smooth geometry, controlled polish, and a design language that benefits from crisp highlights. It can look impressive on front-facing emblems, award tops, and simple bevels, but it is less forgiving on irregular surfaces where tiny marks may become obvious under strong light.
Satin effects are often preferable where buyers want a premium metal appearance with lower emphasis on mirror reflection. They can help create contrast between adjacent areas and may make some handling marks less visually dramatic during inspection, although acceptance standards still need to be defined.
Antique finishing works visually by increasing contrast between raised and recessed details. The effect is strongest when recesses are deep enough to retain darker tone while raised areas can be polished or highlighted cleanly. If a design has very shallow detail or broad undefined textures, antique treatment can lose clarity. This is why early sculpting decisions matter.
When selecting electroplating options or comparing plating finish choices, sourcing teams should ask a specific question: which boundaries and recesses are truly manufacturable? Boundaries with clear geometry, stable edges, and accessible polishing or masking zones are generally more controllable than vague transitions across compound curves, highly textured backgrounds, or narrow slots that are hard to reach and inspect.
Design drawings or marked renderings should identify each finish zone before sampling. A simple annotated image can prevent confusion about whether a border is bright metal, satin metal, antique-highlighted metal, or a painted recess framed by plated edges.
Plating decision framework
| Appearance goal | Best suited geometry | Main risk | Buyer review point |
|---|---|---|---|
| Bright reflective | Open, smooth, front-facing surfaces | Imperfections become visible | Check reflectivity and scratch visibility |
| Satin contrast | Fields needing softer metal look | Inconsistent texture across zones | Check uniformity under angled light |
| Antique effect | Clear raised and recessed detail | Weak contrast on shallow detail | Check wipe consistency and depth perception |
Apply Paint, Color Accents, and Recess Fill
On custom awards, painted areas on zinc alloy are commonly used for brand colors, logos, background panels, enamel-like accents, or recess fill rather than replacing the metallic appearance across the full part. This approach keeps the premium metal character visible while adding identity, event color, or organizational branding.
Paint compatibility depends on casting condition and any prior decorative steps. If paint is applied beside plated or polished metal, sequence control becomes especially important. Exact paint chemistry, cure conditions, and process order should be confirmed with the manufacturer for the project. Industrial coatings guidance also emphasizes that surface preparation is critical to adhesion and coating life, which is directly relevant to painted zinc alloy awards and selectively painted mixed-finish trophies. Reference: https://www.sherwin-williams.com/painting-contractors/pro-industrial-high-performance-coatings/resources/surface-preparation.
Recess depth, wall angle, corner shape, and edge sharpness are major factors affecting fill cleanliness and color separation. A painted zinc alloy award usually performs best when the color is contained within a well-defined area. Shallow bowls, ragged boundaries, and tiny detached paint pockets are harder to fill consistently and harder to inspect objectively during production.
One practical design strategy is to use surrounding plated metal borders around painted zones. These borders create stronger visual contrast and make transition lines easier to see during final inspection. They also give technicians a clearer geometric stopping point than a purely graphic transition without a physical edge.
When considering paint application methods, buyers should minimize tiny isolated color islands, ultra-fine line art, and ambiguous borders that can vary from part to part. If a logo requires very fine detail, it may be better to convert some areas into raised metal, simplify the color separation, or move the artwork to a separate insert or plate, depending on project goals.
Good paint-zone design practices
- Use recesses or borders to contain color.
- Keep corner shapes inspectable rather than needle-sharp and fragile.
- Allow enough wall angle and depth for clean fill.
- Limit isolated micro-details that are difficult to repeat in volume.
- Specify approved color references during sample review.
Plan Masking and Sequence for Mixed Finishes
A mixed finish trophy may combine bright plating, satin contrast, antique areas, and painted sections on a single zinc casting. This is often achievable, but success depends on sequence planning. Surface prep, base metal finishing, selective masking, decorative treatment, paint application, touch-up, and final protection or assembly can each affect the next process. A design that looks simple in CAD can become difficult if the sequence is not considered from the start.
Mixed-finish design works best when boundaries are built into the geometry rather than relying only on visual transitions. A step, rim, recessed panel, or raised border gives a repeatable masking line and a clear inspection standard. A smooth curved surface with a floating change from satin to paint may look elegant in artwork, but it is far harder to execute consistently on production parts.
Masking feasibility depends on edge definition, access, curvature, and production repeatability. Technicians need to locate the same line every time without guesswork. If the boundary is hidden in a complex curve or broken by sculptural texture, variation is more likely. The best mixed finish trophy concepts use zones that can be prepared, masked, and checked with a practical factory workflow.
A useful buyer tool is a finish compatibility matrix. For each zone, compare intended look, substrate condition, process route, masking requirement, and inspection standard. This converts a subjective design conversation into a manufacturability review.
Finish compatibility matrix
| Zone | Intended look | Substrate requirement | Process concern | Inspection focus |
|---|---|---|---|---|
| Front emblem | Bright plated metal | High polish, stable surface | Scratch visibility | Mirror clarity and defects |
| Background field | Satin or antique contrast | Even texture and detail depth | Consistency across area | Uniform tone and wipe |
| Logo recess | Paint fill | Clear depth and edges | Overflow or thin fill | Color separation and coverage |
| Border line | Clean transition | Sharp, accessible edge | Masking repeatability | Line straightness and buildup |
Simple sequencing diagram for RFQ review
- Confirm design intent and finish map.
- Review casting geometry for polish and masking access.
- Agree substrate preparation priorities by zone.
- Confirm plating or base decorative route.
- Define selective masking and paint sequence.
- Approve sample against written cosmetic criteria.
- Protect finished surfaces during assembly and export packing.
Approve Samples and Inspect Transition Lines
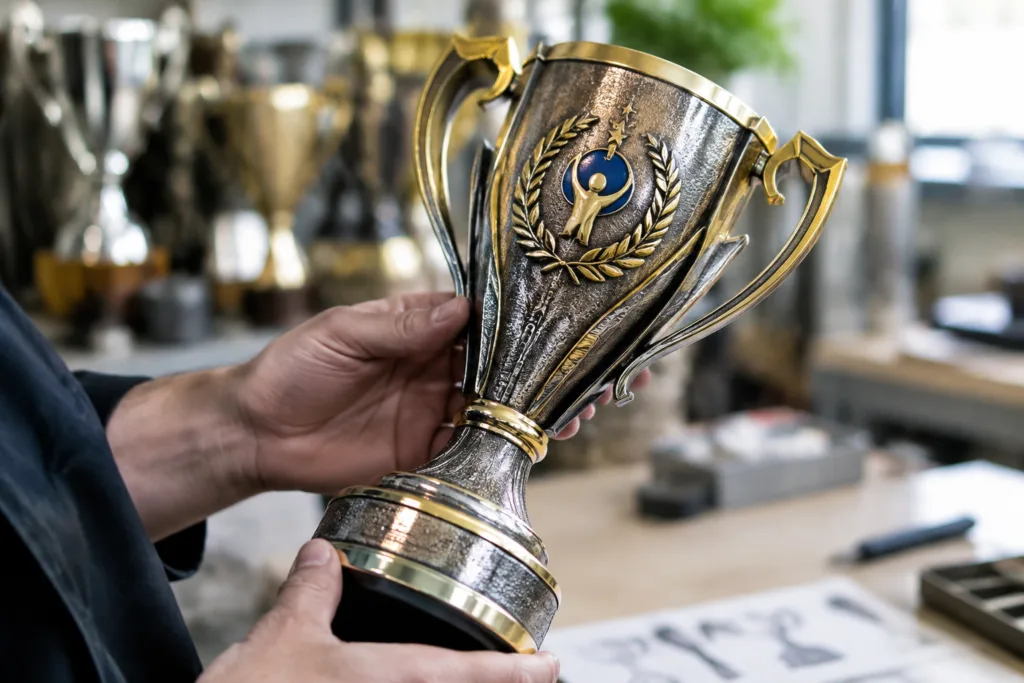
Finish samples and pre-production approval are essential for custom zinc alloy trophies, especially when multiple finish zones must align on one part. Buyers should review more than overall appearance. The critical questions are whether transition lines are clean, whether edge buildup is acceptable, whether color is consistent, whether antique wiping leaves the intended contrast, and whether reflectivity exposes scratches or waviness from likely viewing angles.
A structured finish sample review should include approved reference samples, marked photos, and written cosmetic criteria for mass-production alignment. Exact sampling procedure, approval workflow, and quality checkpoints should be confirmed with Me Trophy for the specific project, particularly when OEM or ODM development involves iterative refinements.
During inspection, compare the part from the primary presentation angle and from secondary handling angles. A trophy may look correct head-on but show weak transition control along side curves or around edges touched during assembly. Procurement teams should also verify which areas are cosmetic and which hidden surfaces can accept natural process evidence, as long as that expectation is documented before production.
Packaging review matters as much as finish approval. Mixed-finish parts can be vulnerable to abrasion at raised plated edges, painted recess rims, and polished highlights. Export delivery planning should therefore include protective packing methods appropriate to the approved finish system; exact packing details should be confirmed for the order.
Checklist for sourcing teams
- Confirm the complete finish map with all zones labeled.
- Define hidden or non-cosmetic areas clearly.
- Identify acceptable natural variation for each finish type.
- Approve color references and antique-tone expectations.
- Review transition-line cleanliness under normal and angled light.
- Check recess wipe quality, paint fill coverage, and edge build-up.
- Confirm packaging protection for plated and painted surfaces during export delivery.
At the finish-sample approval stage, it is also useful to revisit the product pathway for custom zinc alloy trophies so that finish expectations remain aligned with structure, assembly, and export execution rather than being judged in isolation.
Conclusion
Successful zinc alloy trophy finishes depend on matching design intent with casting quality, polish level, and realistic finish sequencing. A single zinc casting can often support plating, paint, antique effects, and mixed-finish zones, but only when geometry, boundary definition, and inspection criteria are designed for manufacturability. For international buyers, the safest path is to evaluate finish compatibility early, convert artwork into a clear finish map, and approve samples against written cosmetic standards.
Me Trophy can support that process as a custom trophy manufacturer and project partner for design-for-finishing review, sample development, OEM or ODM execution, and export-oriented delivery. Project-specific production limits, technical guarantees, and detailed process capability should be confirmed directly for the program.
Related Reading
- when zinc alloy is the right material
- electroplating defect inspection guide
- Pantone matching for painted metal trophies
- die-cast trophy sample review
- custom trophy inspection checklist
FAQs
Can one zinc alloy casting support plating and paint on the same trophy?
Often yes, if the design provides clear physical boundaries, stable edges, and zones that can be polished, masked, and inspected consistently. Feasibility should be confirmed with the manufacturer during sample development.
What makes a zinc trophy antique finish look clean rather than muddy?
Clear raised and recessed geometry is the main factor. Antique effects work best when recesses hold darker tone while raised areas remain well defined after polishing and wiping.
Why is surface preparation so important for a painted zinc alloy award?
Preparation affects adhesion, edge cleanliness, and final appearance. Deburring, smoothing, and cleaning must match the intended paint zone and any adjacent plated surfaces.
Are mixed finish trophy boundaries better as visual artwork or built into the casting?
Built-in geometric boundaries such as recesses, rims, and raised borders are usually easier to mask, repeat, and inspect than purely visual transitions across curved surfaces.
What should buyers approve before mass production of zinc alloy trophy finishes?
Buyers should approve the finish map, reference sample, color references, acceptable natural variation, transition-line quality, and packaging protection method for export delivery.