A trophy pilot order is the stage that turns an approved sample into evidence that a new overseas supplier can produce consistently under realistic batch conditions. A hand-approved sample may look correct, but it does not automatically prove stable die-casting, repeatable polishing, controlled plating, accurate paint application, secure assembly, reliable packaging, or disciplined shipment preparation. For procurement teams onboarding a new manufacturer, this is where sourcing risk reduction becomes practical rather than theoretical. When buyers review capability fit, process flow, and project control logic, it helps to start with a metal trophy manufacturing overview so the pilot is designed around real factory stages instead of showroom expectations.
In custom trophy sourcing, the gap between sample approval and bulk order confidence is usually caused by process variation. Fine logos may soften in casting, mirrored surfaces may reveal polishing inconsistency, electroplated finishes may shift in tone, paint lines may drift, inserts may loosen during assembly, and cartons that looked acceptable in a courier sample may fail in export handling. A controlled custom trophy trial order should therefore be built to answer one core question: can this supplier repeat the approved standard under batch conditions, with the documentation, communication, and packaging controls needed for scale?
This article gives procurement managers a practical framework for new trophy supplier qualification. It focuses on representative product selection, frozen specifications, milestone inspection, packaging validation, communication routines, and measurable go or no-go criteria. It also explains how a manufacturing partner such as Me Trophy can support pilot execution, capability alignment, and production control planning for custom metal trophy projects, while noting that any company-specific operating details should be confirmed for the project.
Decide What the Pilot Must Prove
The pilot should validate production repeatability, not simply confirm that one approved sample exists. Procurement teams often fall into a common trap: they treat a pilot as a mini order whose only purpose is to obtain goods. A better approach is to define the pilot as a controlled test of the supplier’s ability to hold standard across manufacturing steps and across units.
Start by separating pilot objectives into four categories:
- Quality: repeatable dimensions, finish consistency, logo clarity, assembly fit, and cosmetic workmanship.
- Delivery: milestone adherence, documentation timing, shipment readiness, and issue recovery speed.
- Communication: update frequency, escalation discipline, change control, and responsiveness to questions or deviations.
- Packaging: individual protection, anti-scratch measures, insert fit, carton labeling, and export handling readiness.
This structure prevents the pilot from becoming a subjective beauty contest. It also helps answer the procurement question: Is the pilot representative enough to predict bulk order performance? If the run does not test likely failure points, it cannot predict bulk performance. If it does not test communication and document control, it cannot predict scaling behavior. If it does not test packaging in packed-carton condition, it cannot predict export arrival condition.
A practical method is to build a weighted pilot scorecard before production starts. For example, buyers can assign greater weight to finish consistency, assembly stability, packaging protection, and schedule reliability than to less critical points. Exact score thresholds should be defined by the buyer’s program requirements, but the logic should be simple:
| Category | What to Measure | Typical Evidence | Go/No-Go Logic |
|---|---|---|---|
| Quality | Visual consistency, dimensions, logo accuracy, assembly security | Inspection report, reference photos, retained samples | Critical defects not acceptable; repeatability must be demonstrated |
| Delivery | Milestone completion and shipment readiness | Production timeline, dated updates, packing completion status | Major schedule slippage requires review of root cause and recovery capability |
| Communication | Response speed, clarity, revision control, escalation quality | Email trail, approval records, issue logs | Uncontrolled changes or unclear ownership are strong risk signals |
| Packaging | Protection, labeling, carton integrity, handling suitability | Packing sample, drop or transit review if agreed, packed photos | Damage risk or unclear labeling blocks scale-up until corrected |
Formalize the outcome in a go/no-go review. If the supplier passes only because the buyer verbally waives multiple issues, then the pilot has not truly reduced risk. The point is not to punish normal pilot findings; it is to convert findings into measurable controls before volume commitment.
Choose Representative Products, Finishes, and Packaging
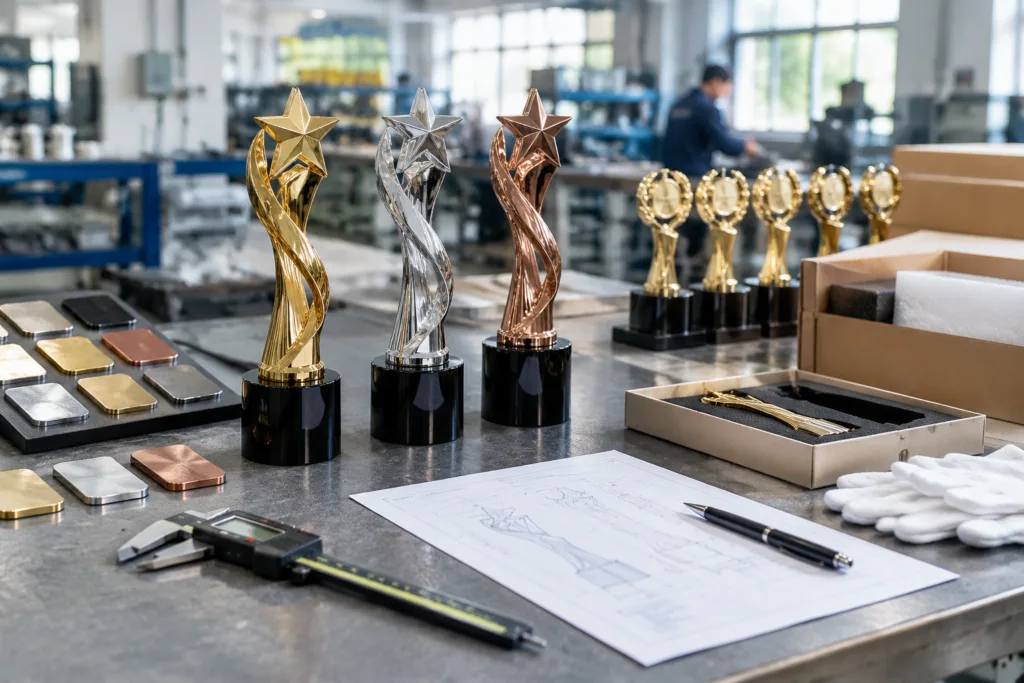
The best pilot order is not the easiest SKU. It is the most representative test of your future production reality. If your program includes multiple components, custom bases, fine lettering, plated metal surfaces, painted areas, or mixed-material assemblies, at least one pilot SKU should reflect those complexities. A simplified display sample can hide exactly the process weaknesses that cause problems later.
When planning supplier pilot production, include combinations that are known to be failure-prone in custom metal trophies:
- Sharp raised or recessed details that challenge casting and polishing
- Mirrored metal surfaces that expose scratches and waviness
- Electroplated finishes where color tone and coverage must stay consistent
- Color-filled logos or painted recesses where edge definition matters
- Long or fragile protruding features that can bend or chip in packing
- Multi-part assemblies with posts, screws, adhesive points, or insert fit
- Custom bases where flatness, logo placement, and assembly alignment affect presentation
Packaging should be validated with the same discipline as the product itself. A pilot should confirm:
- Whether each unit has sufficient inner protection against abrasion
- Whether anti-scratch bagging, foam, tissue, or partitions are appropriate
- Whether protruding elements are immobilized or buffered
- Whether gift boxes, inner boxes, and master cartons fit the product correctly
- Whether labels, carton marks, and count accuracy support warehouse receiving and export shipment handling
This is why the pilot should mirror realistic batch conditions rather than a showroom-style hand-picked run. For buyers moving from trophy sample to bulk order, the real question is not whether one display-quality piece can be made. It is whether a packed batch can be made with stable workmanship and predictable handling outcomes.
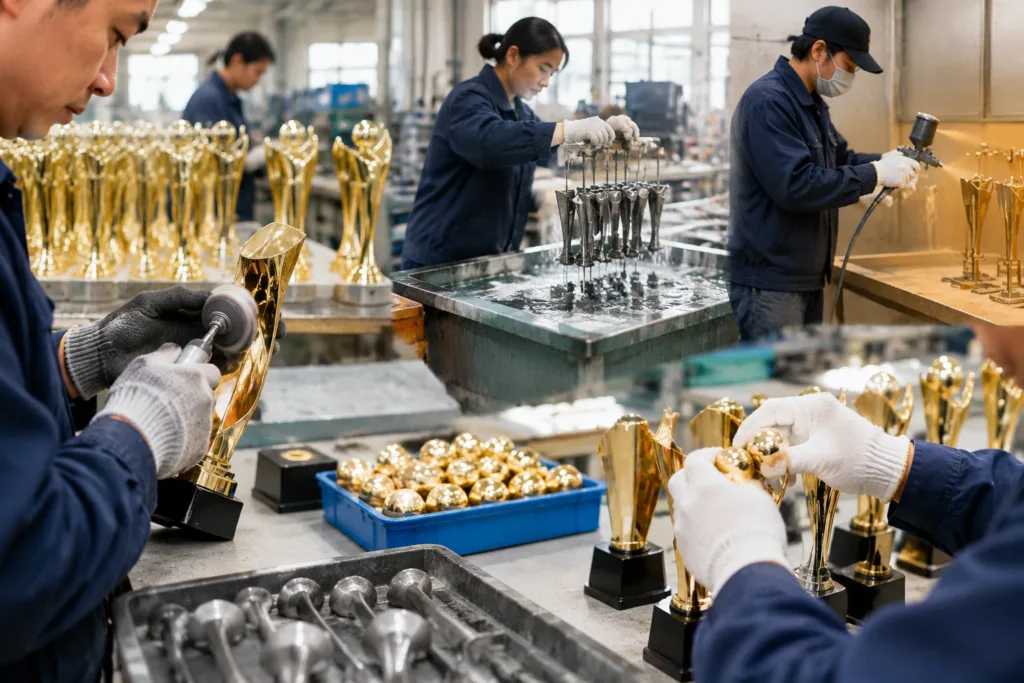
During supplier-fit evaluation, capability alignment matters. Buyers should understand whether the factory can manage relevant processes in sequence, including die-casting, polishing, electroplating, painting, assembly, inspection, and shipping preparation. Me Trophy presents itself as a manufacturing partner for custom projects, and buyers can review its OEM trophy manufacturing approach alongside the earlier metal trophy manufacturing overview when assessing fit. Company-specific workflow depth, process ownership, and project arrangements should still be confirmed directly for the pilot.
Freeze Specifications and Approval Masters
Many pilot failures are not factory capability failures alone. They are specification failures. If the drawing says one thing, the approved sample suggests another, the artwork file is revised informally, and the packaging note is buried in email, the supplier may produce exactly what the documentation allows while the buyer still feels the result is wrong.
Before launching the pilot, freeze the full specification set:
- Approved drawings and key dimensions
- Material callouts where applicable and to the level confirmed for the project
- Finish references for plating, polishing level, texture, and sheen
- Color standards for painted areas and fills
- Artwork files, logo size, orientation, and placement rules
- Assembly method, including fasteners, adhesives, inserts, or base attachment
- Labeling rules, barcode placement if applicable, and carton marks
- Packing instructions down to inner protection and carton pack-out configuration
Equally important are approval masters. A pilot should not rely on memory or scattered attachments. Maintain a controlled set of references such as:
- A signed or clearly approved production sample
- A finish swatch or metal reference sample where relevant
- An approved packaging sample or mock pack configuration
- Defect boundary examples showing what is acceptable, reworkable, or rejectable
Version control should cover bill of materials, artwork, labels, cartons, inserts, inspection criteria, and any revision notes. If a new logo file or carton dimension is introduced during the pilot, all stakeholders should see the same revision status. This is where many transitions from trophy sample to bulk order break down: the buyer believes the visual approval is frozen, but the production team is working from mixed versions.
If molds are involved, mold readiness should also be treated as a controlled deliverable rather than an assumption. Buyers should understand whether tooling has been finalized, what signoff is required before production release, and what dimensional or detail-sensitive areas need first-off attention. For projects requiring new tooling, a structured review of mold development can help frame the pilot plan, although project-specific tooling details must be confirmed directly.
Likewise, when pilot pieces are created through a formal sample production route before release to batch manufacturing, procurement should ensure the sample and pilot share the same approved references. A beautiful sample made under special handling is not enough if the batch specification package is incomplete.
Set Communication, Inspection, and Escalation Rules
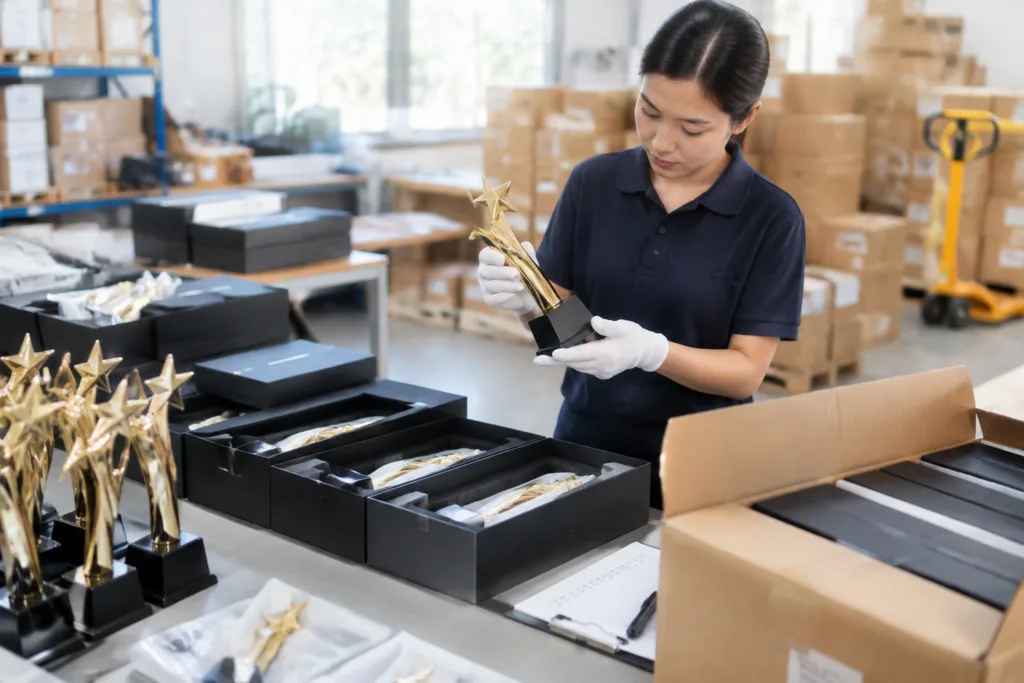
A pilot order should have a communication routine just as structured as the manufacturing plan. Define who at the buyer approves changes, who receives updates, and what kind of issue requires explicit signoff before production continues. Without this, suppliers may solve problems informally in ways that create new deviations.
At minimum, define:
- Approval authority: who can release drawings, approve cosmetic waivers, or accept schedule adjustments
- Update rhythm: daily brief updates or milestone-based reports depending on pilot size and complexity
- Photo requirements: what images are needed at first-off, in-process, packing, and pre-shipment stages
- Stop rules: which defects or changes require production hold pending buyer review
- Escalation contacts: who acts when plating variation, missing parts, schedule slippage, or carton failure appears
Milestone checks are especially useful in custom trophy manufacturing because visible defects often originate earlier in the process. Consider setting checkpoints at these stages:
- Mold readiness or tooling signoff where applicable
- First-off castings or first assembled article review
- Pre-plating review for surface preparation and defect visibility
- Pre-paint review for masking, recess quality, and edge clarity
- Assembly verification for fit, stability, and orientation
- Packed-unit review and pre-shipment inspection readiness
Buyers should also document an agreed inspection method. Exact acceptance plans should be confirmed by the buyer and supplier, but the principle is simple: define how finished goods will be checked, what constitutes critical, major, or minor concerns for the project, and whether random sampling or 100% checks are required for certain attributes. Intertek’s guidance on inspection services notes that pre-shipment inspection is typically performed when goods are completed, packed, and ready for shipment, and that random sampling can be based on recognized methods such as ANSI/ASQ Z1.4 and ISO 2859, which is useful context for pilot exit planning and later scale-up discipline: pre-shipment inspection using recognized AQL sampling methods.
Escalation triggers should be explicit. Examples include:
- Cosmetic defects exceeding the approved boundary examples
- Plating variation visible between units or lots
- Paint adhesion concerns, edge bleed, or color drift from reference
- Loose assembly, unstable bases, or missing hardware
- Logo, label, or artwork mismatches
- Packing failures such as carton crush risk, insufficient cushioning, or mixed labels
- Any milestone slip that threatens agreed shipment timing
Me Trophy can be positioned here as a project partner capable of coordinating checkpoints across mold development, casting, polishing, plating, painting, assembly, inspection, and packaging, with company-specific workflow and reporting details to be confirmed for each project. For buyers evaluating control discipline, it is reasonable to ask how the supplier’s quality control process aligns with the pilot scorecard and escalation logic.
Review Delivery Performance and Nonconformities
At pilot close, do not review only the finished goods. Review the supplier’s behavior during the project. A supplier that identifies issues early, contains them, communicates clearly, and implements corrective action may be a better long-term partner than one that ships acceptable pieces after hiding rework and drifting off schedule.
Evaluate delivery performance against the plan:
- Were milestones met as agreed?
- Was documentation clear, complete, and timely?
- Did the supplier answer questions quickly and directly?
- Were deviations escalated before they became shipment problems?
- Was the order fully ready for dispatch with correct packing and shipping documents?
Then review nonconformities by defect type, not as one blended defect count. For custom trophies, category-level analysis is more useful than a simple pass rate. Typical review buckets include:
- Surface flaws such as scratches, pits, polishing marks, or dents
- Color inconsistency in painted areas or filled logos
- Dimension mismatch affecting fit or appearance
- Assembly looseness, leaning components, or detached parts
- Logo or artwork errors, including orientation and placement mistakes
- Plating defects such as tone variation, thin coverage, stains, or edge problems
- Paint adhesion concerns or finish fragility requiring further validation
- Packaging damage, abrasion, crushed inserts, or carton labeling errors
It is important to judge problem-solving behavior, not only defect counts. A new trophy supplier qualification decision should consider whether the supplier can isolate root cause, contain suspect stock, and prevent recurrence. A structured post-pilot review can follow this sequence:
| Review Step | What to Ask | Expected Output |
|---|---|---|
| Root cause | Why did the issue happen at the process level? | Cause statement linked to casting, polishing, plating, painting, assembly, or packing stage |
| Containment | How was affected product identified and separated? | Sorting, re-inspection, hold status, and stock traceability |
| Corrective action | What was changed to fix the current pilot? | Immediate action with responsibility and completion evidence |
| Preventive action | How will recurrence be reduced in future production? | Updated control point, training note, work instruction, or inspection method |
| Ownership | Who is accountable for follow-through? | Named owner, due date, and verification method |
Which success criteria must be met before scale-up? That depends on the buyer’s risk profile, but some criteria are usually non-negotiable: no unresolved critical quality issues, stable visual standard across inspected units, packaging that protects the product in packed condition, controlled documentation, and communication behavior consistent with future program needs. If shipment preparation is part of the pilot scope, buyers should also confirm that the supplier can support reliable packaging and export delivery execution for the product configuration tested.
Convert Lessons Into Full-Order Controls
A pilot reduces risk only if its lessons become standard controls for the bulk order. Too often, teams complete a trial, discuss findings informally, and then issue a larger purchase order without revising the specification pack. That throws away the value of the pilot.
Use pilot findings to update the operating package for future orders:
- Retain golden samples for product and packaging references
- Add process checkpoints at the stages where defects were found or prevented
- Clarify packaging instructions with photos, pack-out counts, and protection details
- Define inspection plans for appearance, assembly, labeling, and packed-carton status
- Require photo reports at agreed milestones
- Document change-control rules so no revision is implemented without approval
- Update purchase specifications and any supplier quality agreement language based on actual pilot evidence
There are also cases where immediate scale-up is not the right next step. A second pilot or limited rollout is often wiser when:
- The supplier met cosmetic targets but schedule control was weak
- Packaging was revised late and not fully validated under packed conditions
- One finish, color, or assembly type remains unstable
- Corrective actions were proposed but not yet proven in production
- The pilot SKU was representative but did not cover all high-risk variants
For procurement teams, a practical go/no-go template should cover four areas: quality repeatability, schedule reliability, communication discipline, and packaging performance. A supplier may still be approved with open actions if those actions are clearly owned, time-bound, and low risk to scale-up. But unresolved instability in finish consistency, assembly security, or packaging protection should usually trigger either another pilot or a limited commercial release rather than full volume.
When planning pilot execution and conversion to volume controls, buyers may also use the supplier’s manufacturing flow as a discussion framework. Me Trophy can be approached as a manufacturing project partner for capability alignment, pilot checkpoint planning, and cross-process coordination from casting through finishing and assembly to shipment readiness. Buyers considering this route can revisit the metal trophy manufacturing overview as a reference point for those commercial and technical discussions, while confirming all project-specific operating details directly.
Recommended downloadable asset: a pilot scorecard and go/no-go review template tailored for custom trophy sourcing. At minimum, it should include weighted criteria, defect category logs, milestone tracking, packaging validation fields, corrective action ownership, and a final recommendation section.
A well-designed trophy pilot order reduces onboarding risk because it turns assumptions into measurable controls before the bulk commitment is made. For overseas buyers, that is the real bridge between an approved sample and confident volume release.
Practical FAQs
1. What quantity should a trophy pilot order include?
The quantity should be large enough to test repeatability, packing, and communication discipline under batch conditions, but the exact size must be defined by the buyer’s risk level, SKU complexity, and project budget. It should be confirmed with the supplier rather than assumed.
2. Should the pilot use the hardest SKU or the highest-volume SKU?
Ideally, include the SKU or combination of features most representative of future production risk. If one item carries the highest cosmetic or assembly complexity, that often provides better qualification value than the easiest high-volume item alone.
3. What should block scale-up after a custom trophy trial order?
Common blockers include unresolved critical defects, unstable finish consistency, poor revision control, weak issue escalation, repeated packing failures, or a shipment that was not truly ready according to agreed requirements.
4. How do buyers connect sample approval to bulk order control?
Freeze approval masters, version-controlled drawings, finish references, packaging instructions, and inspection criteria before pilot launch. Then convert pilot findings into standard checkpoints, photo-report requirements, and change-control rules for the bulk order.
5. When is a second pilot better than a full rollout?
A second pilot is often the safer option when corrective actions have been proposed but not yet proven, when packaging changed late, when one finish or assembly type remains unstable, or when the first pilot did not cover enough real production complexity.